Red Light Manufacturer | OEM LED Solutions

red light manufacturer

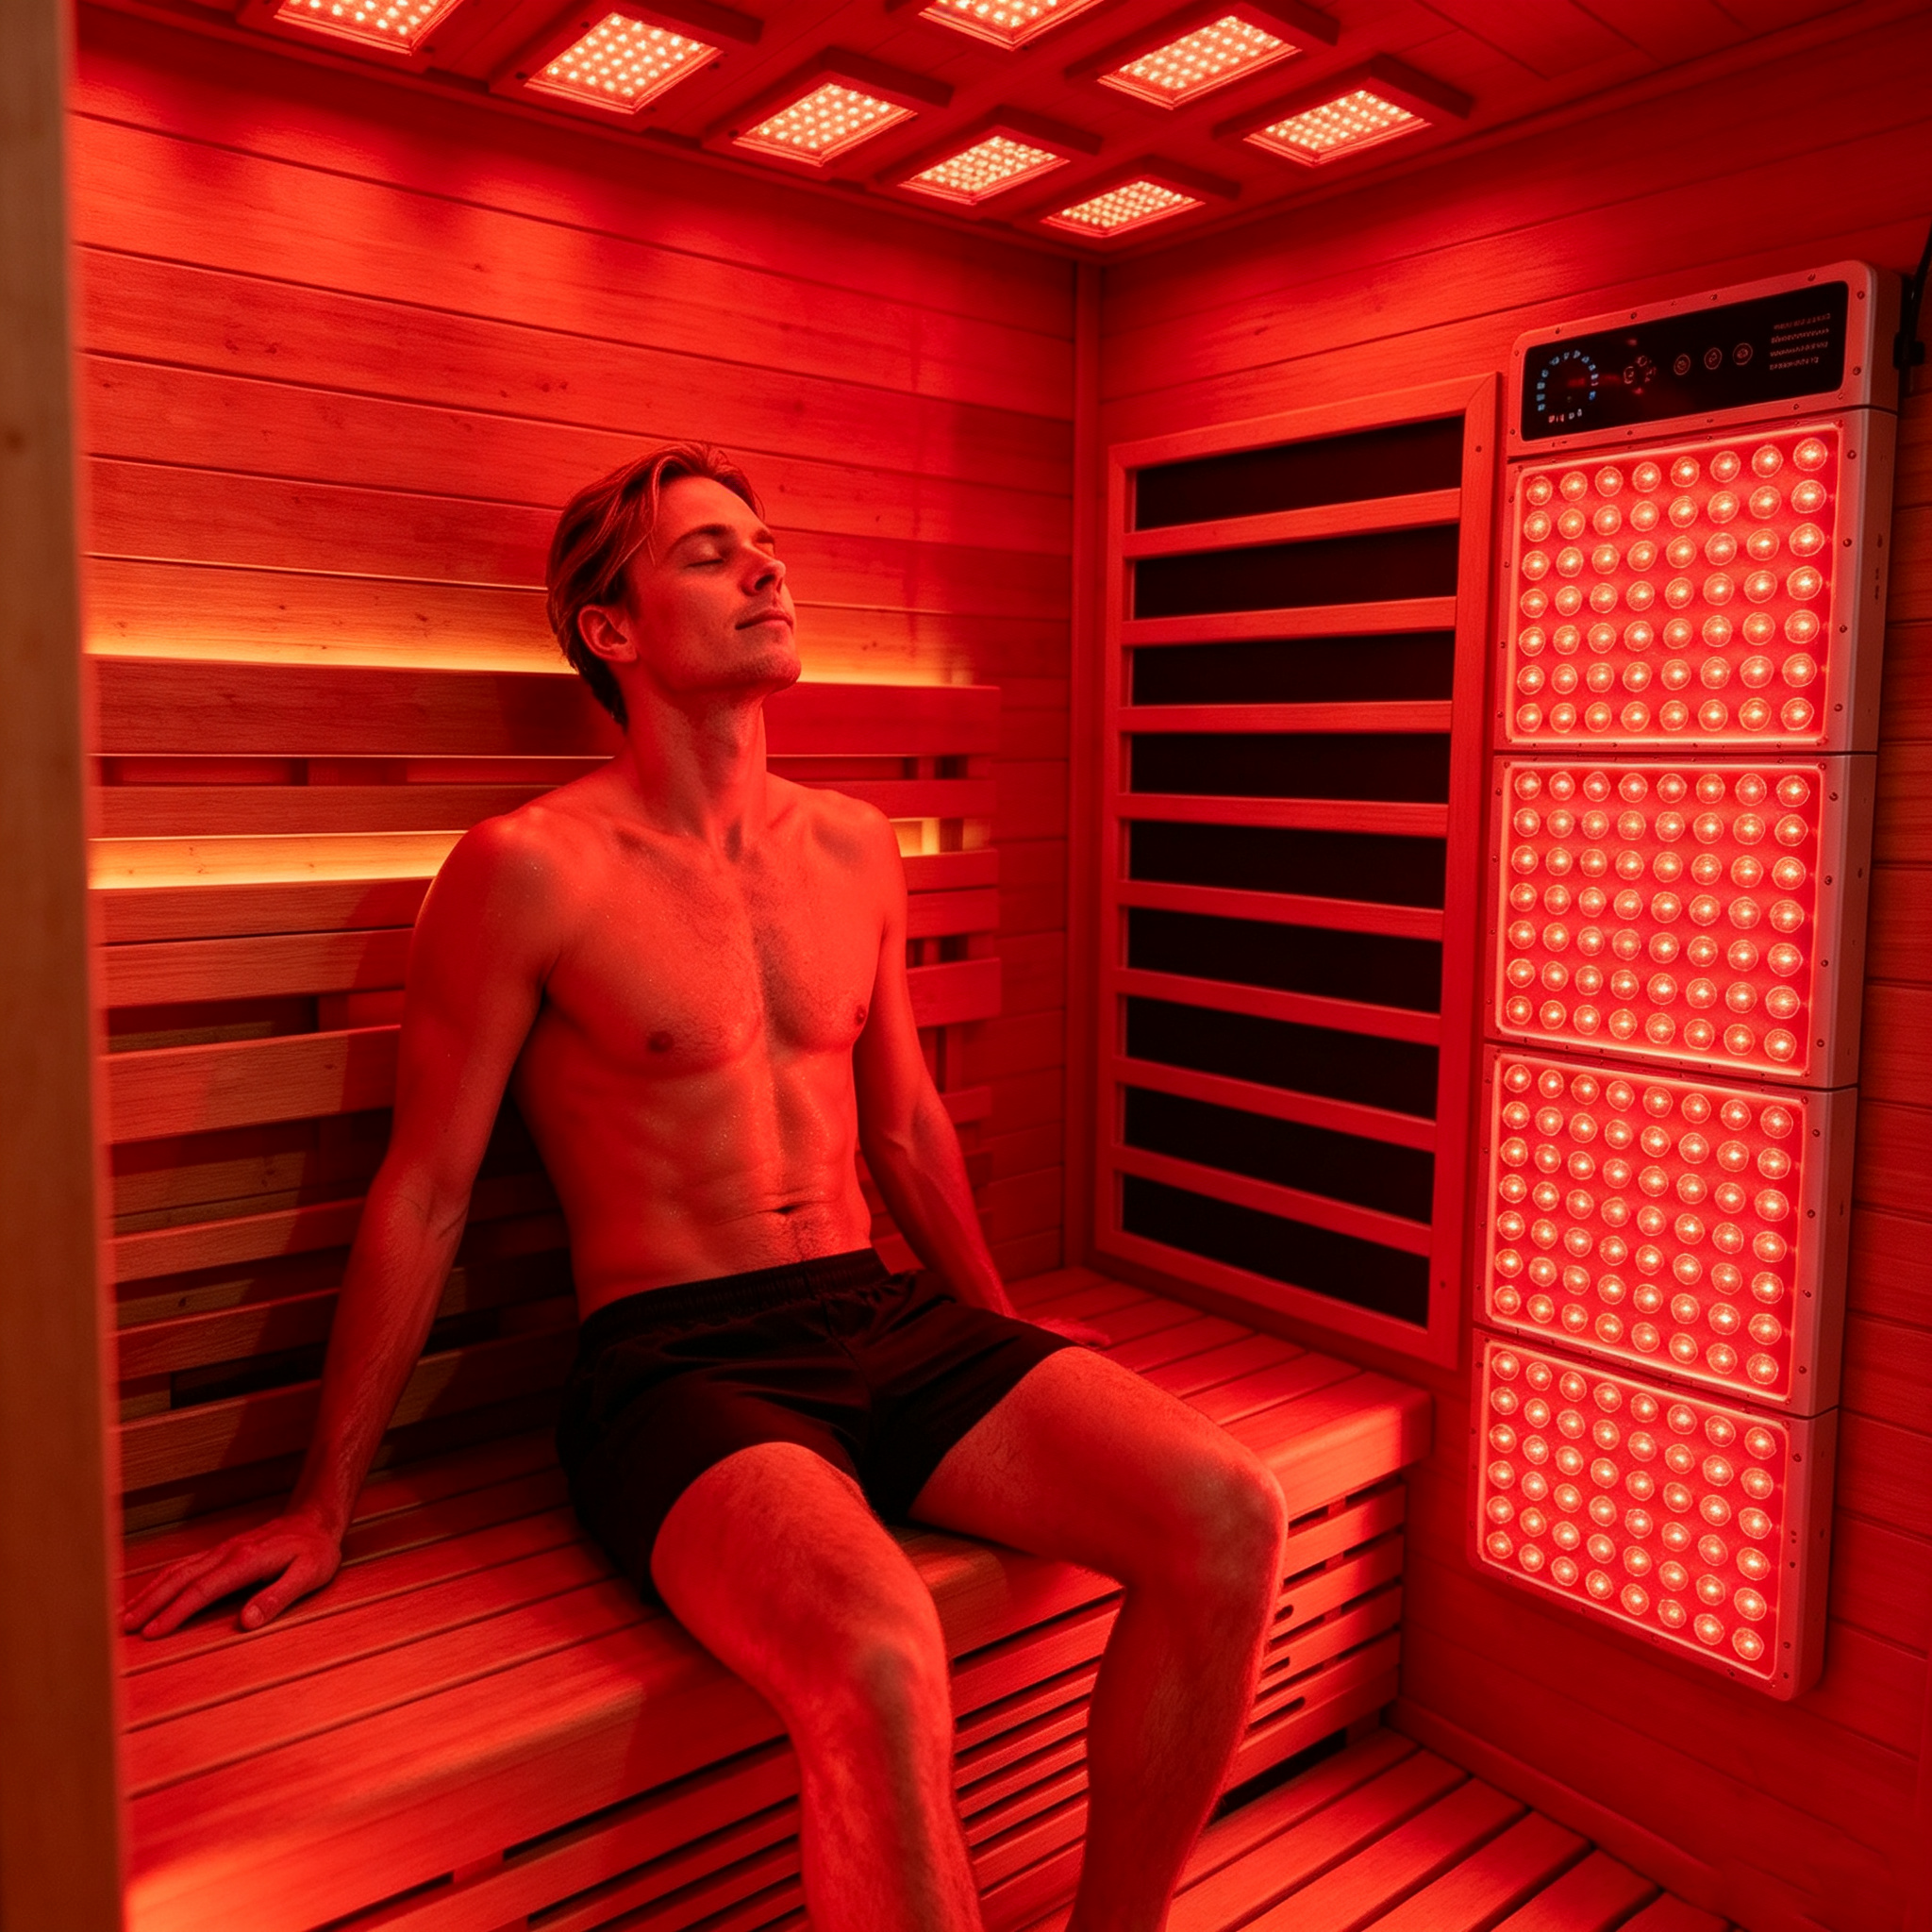
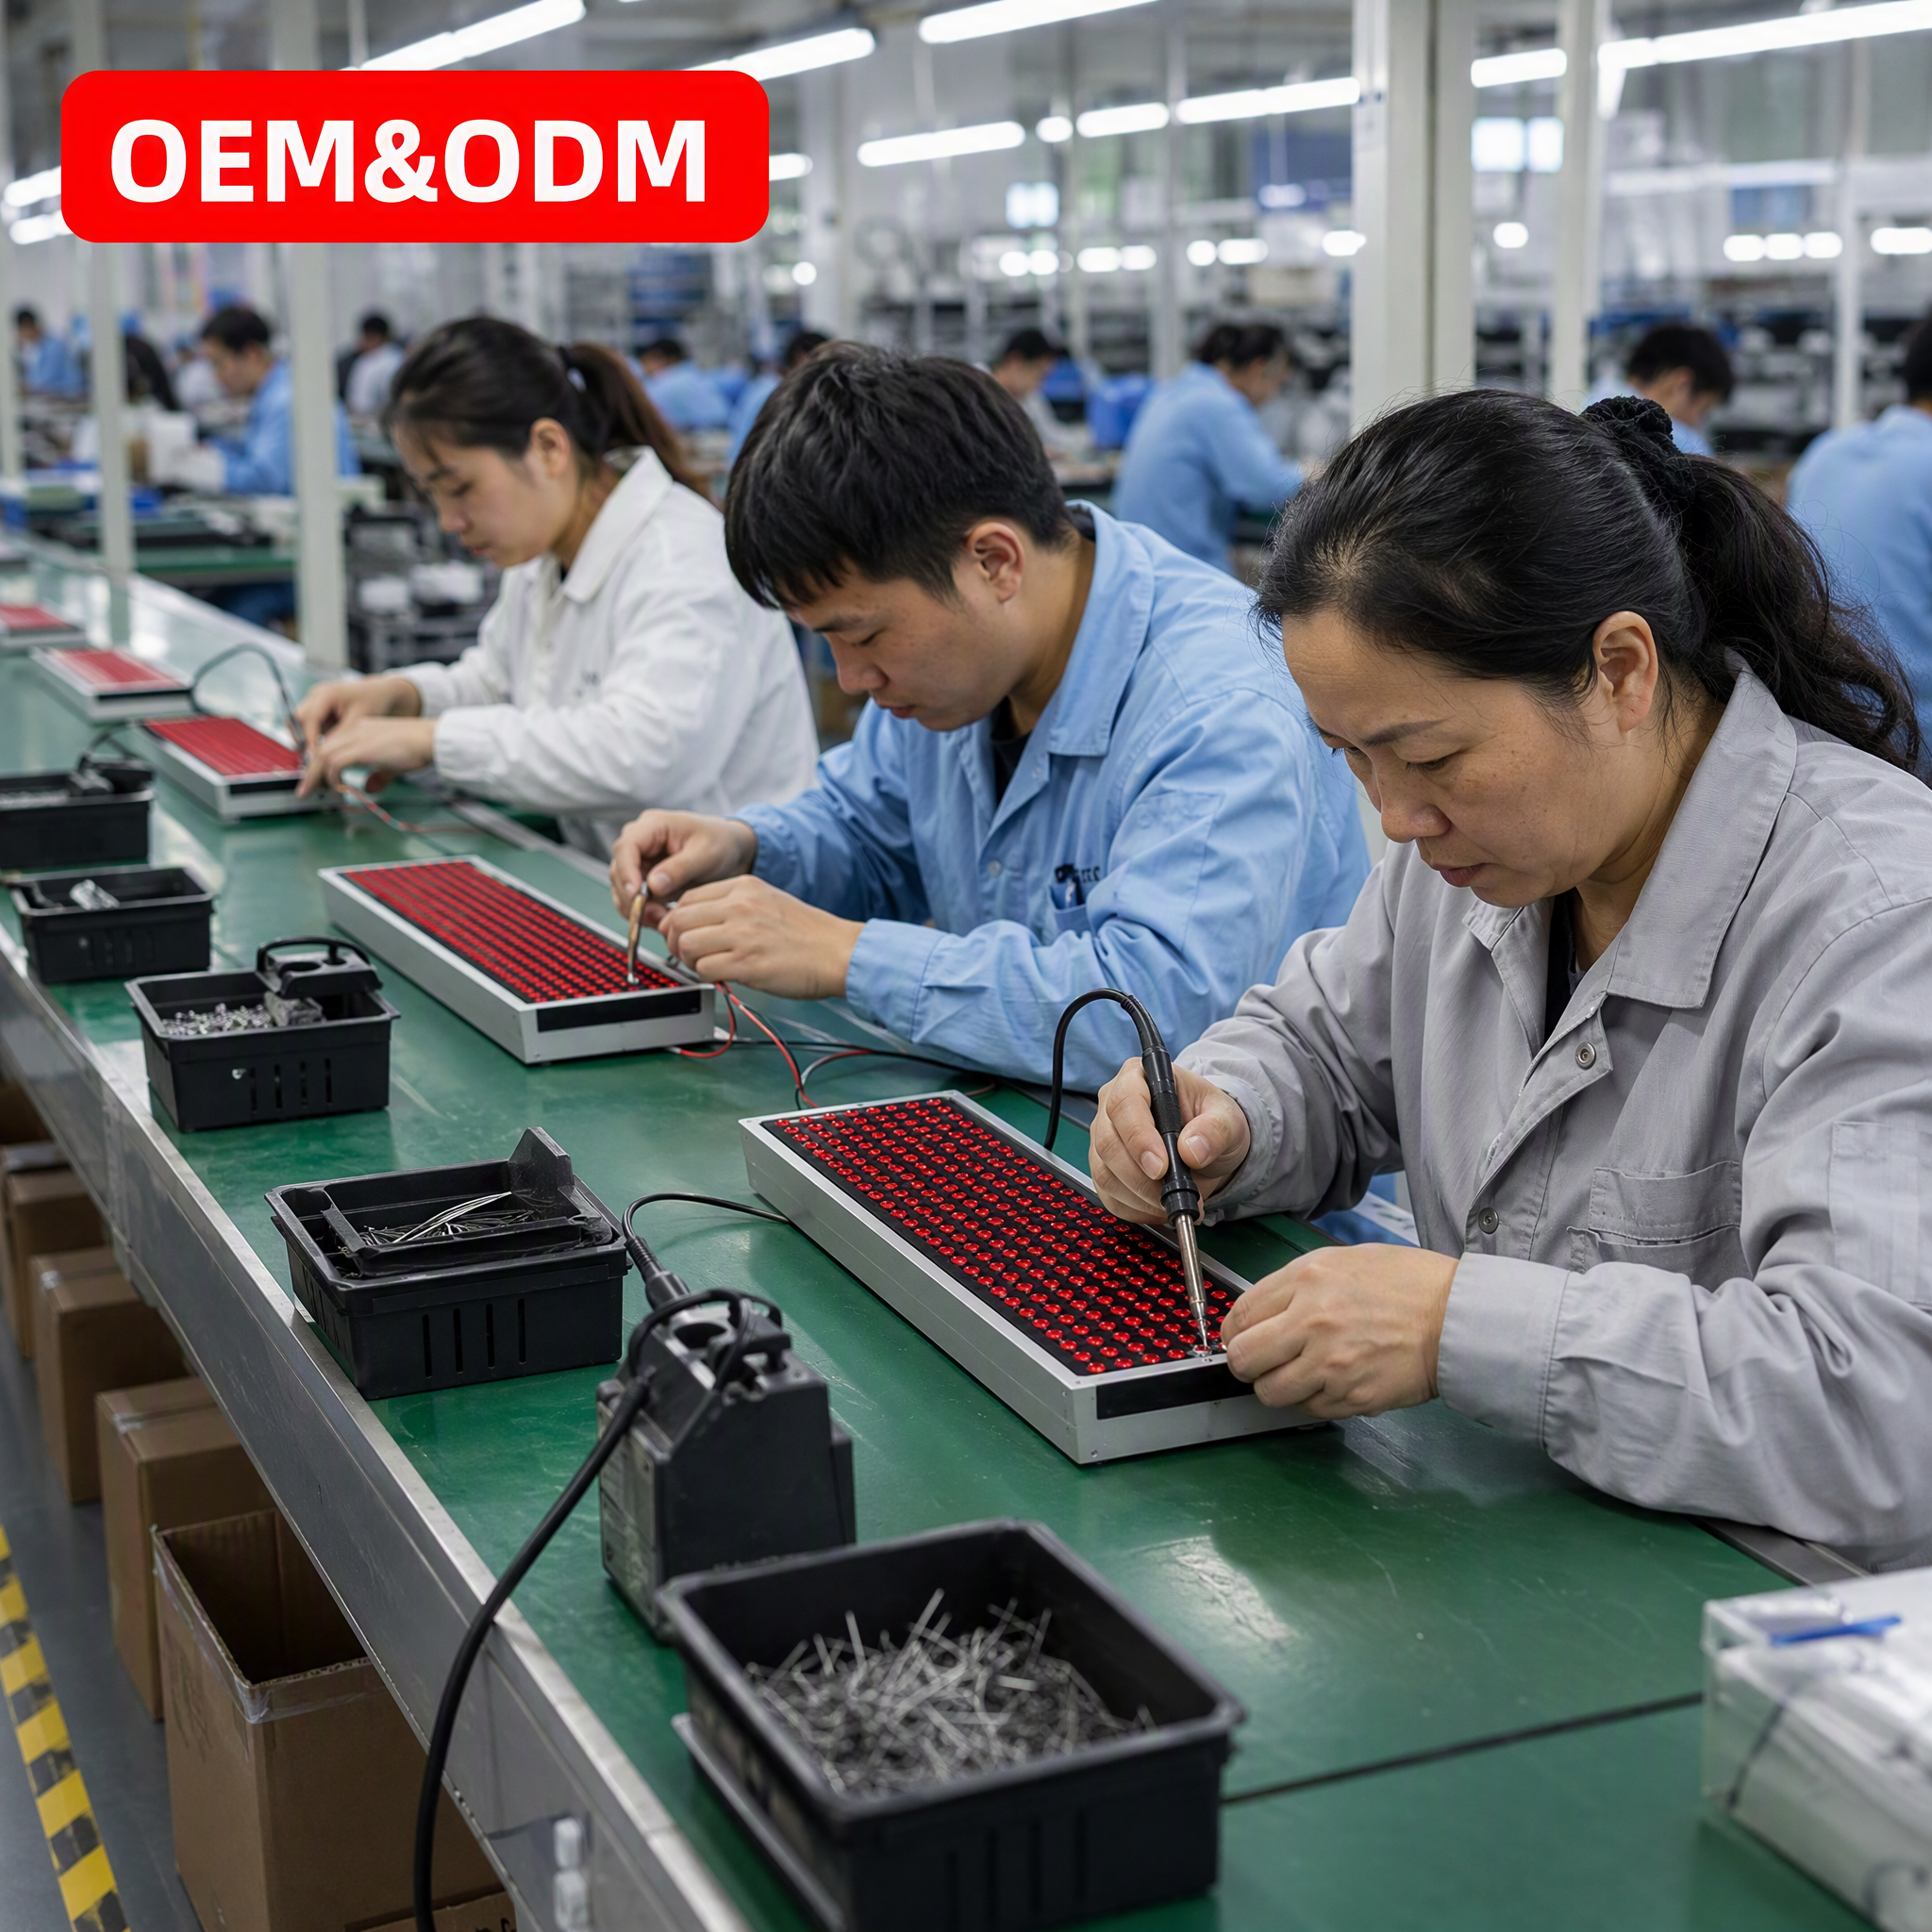
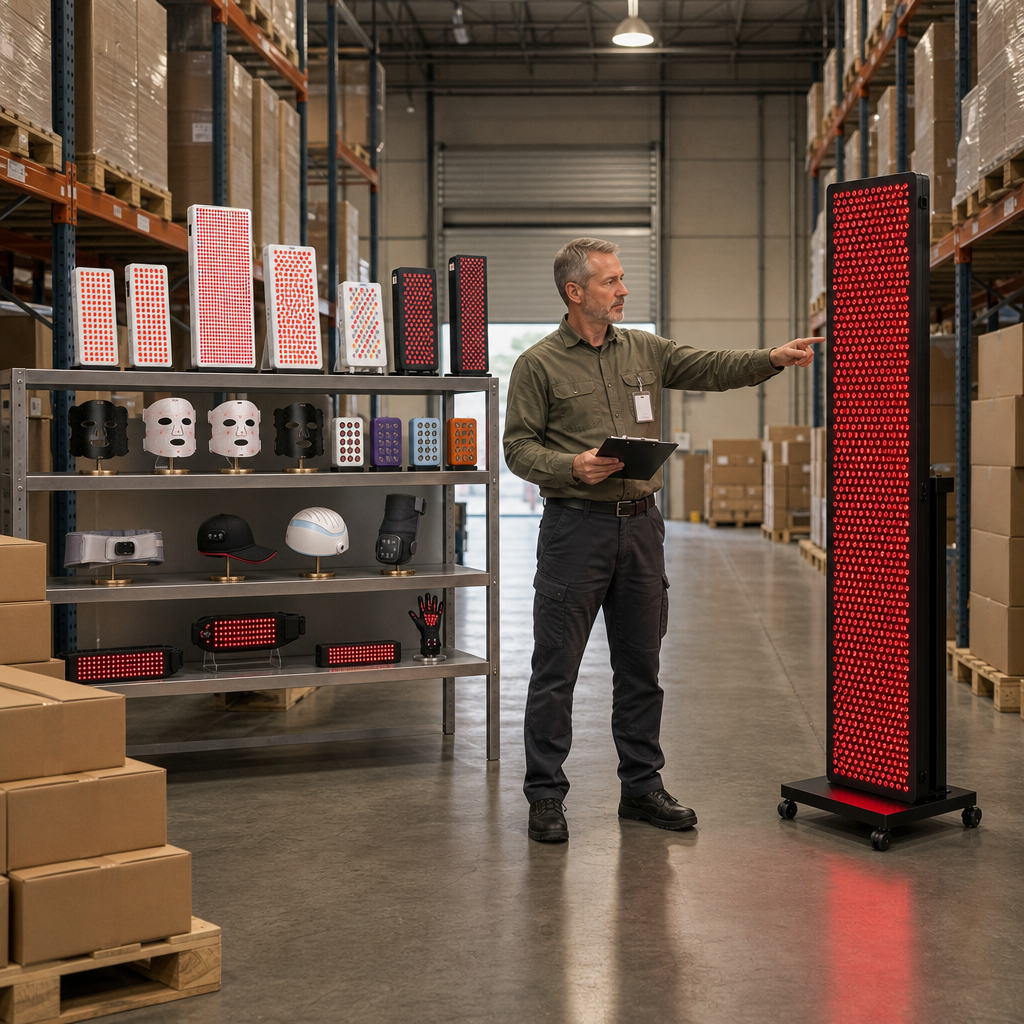
A red light manufacturer designs, develops, and produces red LED lighting equipment for commercial, industrial, medical, beauty, and consumer use. The right red light manufacturer manages the full process, from selecting LED chips and creating optical layouts to assembling housings, testing performance, and preparing products for delivery. This complete approach helps buyers source dependable equipment from one experienced partner. Most products supplied by a red light manufacturer use efficient LED technology to produce controlled wavelengths, stable output, and low heat. Depending on the model, systems may include adjustable intensity, programmable timers, cooling fans, touch controls, remote operation, and safety sensors. A capable red light manufacturer can also offer panel lights, handheld devices, flexible strips, tunnel systems, and custom fixtures for different installation conditions. The main function of a red light manufacturer is to turn a specific lighting need into a practical product. A manufacturer can support therapy equipment, skin care tools, plant growth systems, inspection lights, signage, displays, and specialty illumination. The red light manufacturer may provide standard products for fast purchasing or create OEM and private-label designs for brands that need a distinct appearance or operating format. Quality control remains central to every red light manufacturer. Production checks can cover wavelength accuracy, brightness, electrical safety, heat management, durability, and long-term operation. Buyers can also request packaging, branding, certifications, user instructions, and sample testing. By working with a red light manufacturer that combines engineering, production, and support, customers gain a clearer route from concept to reliable finished product.
Popular Products

Choosing a red light manufacturer gives buyers direct access to product knowledge, production control, and practical customization. Instead of adapting a general lighting product, a customer can explain the target use, working distance, coverage area, control method, and budget. The red light manufacturer can then recommend a suitable size, wavelength, power level, and housing style. This reduces guesswork and supports a better match between product and application. A major buyer benefit is consistent supply. A professional red light manufacturer uses defined materials, assembly steps, and inspection procedures across production batches. Consistency helps brands protect product performance, reduce customer complaints, and plan repeat orders with greater confidence. It also makes it easier to compare samples with later shipments. For businesses selling equipment under their own name, the red light manufacturer can support branded labels, custom colors, packaging, manuals, and accessories. Operational efficiency is another advantage. A red light manufacturer that handles design, sourcing, assembly, testing, and shipping can reduce the number of outside suppliers involved in a project. Fewer handoffs may shorten communication time and make problem solving more direct. Buyers can also discuss volume pricing, spare parts, replacement units, and production schedules with one contact. Application suitability matters just as much as price. A red light manufacturer can adapt beam spread, mounting options, controls, protection levels, and cooling methods for clinics, salons, farms, laboratories, retail spaces, workshops, or home use. Buyers should ask about output data, safety testing, warranty terms, minimum order quantities, and lead times before placing an order. This information helps compare suppliers on total value rather than purchase price alone. Finally, an experienced red light manufacturer can support growth. A business may begin with a small sample order, verify market response, and then scale production without changing the core design. Technical guidance, responsive service, and documented quality checks give customers useful confidence throughout the purchasing process.

Tips And Tricks

What Is Medical Red Light Technology and Where Is It Commonly Used?

29

Oct

What Is Medical Red Light Technology and Where Is It Commonly Used?

Medical red light technology has emerged as a powerful therapeutic tool in modern healthcare, offering non-invasive solutions for tissue healing and cellular regeneration. This sophisticated approach leverages specific light wavelengths to stimulate ...
View More
What Safety Controls Should an Infrared Sauna Blanket Include?

15

Oct

What Safety Controls Should an Infrared Sauna Blanket Include?

Selecting an infrared sauna blanket requires careful evaluation of built-in safety controls to protect users during sessions. An infrared sauna blanket emits far-infrared wavelengths that penetrate skin tissue, triggering therapeutic responses throug...
View More
What Safety Features Should Buyers Check in Laser Therapy Devices?

22

Oct

What Safety Features Should Buyers Check in Laser Therapy Devices?

When selecting laser therapy equipment, understanding critical safety features is essential to ensure both patient protection and regulatory compliance. Medical professionals and facility operators must carefully evaluate devices before purchase to a...
View More
What Should Pet Owners Consider When Choosing Red Light Devices?

08

Oct

What Should Pet Owners Consider When Choosing Red Light Devices?

Pet owners increasingly recognize the therapeutic potential of red light devices for their animals, but selecting the right system requires understanding several critical factors. Whether you're considering pet red light therapy for pain relief, woun...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Mobile
Message
0/1000

red light manufacturer

Custom Design for Different Operating Needs

Custom Design for Different Operating Needs

A strong red light manufacturer does more than offer a fixed catalog. It listens to how the product will be used and adjusts the design accordingly. The red light manufacturer may change the light area, LED arrangement, wavelength mix, control panel, cable length, mounting bracket, or outer case. These changes help the final unit fit a treatment room, retail counter, growing shelf, production line, or portable kit. This flexibility creates clear value for buyers. A product that matches its working environment is easier to install, operate, and maintain. Custom design can also improve the appearance of a private-label product and help a brand stand apart from low-cost alternatives. The red light manufacturer can usually review drawings, samples, technical targets, and packaging requirements before mass production. That review gives customers an opportunity to identify design problems early, control development costs, and confirm that the finished equipment supports its intended task. Buyers gain a practical route from idea to market-ready product without building their own production facility.
Stable Output and Careful Quality Control

Stable Output and Careful Quality Control

Performance consistency is a key reason to work with an established red light manufacturer. Each red light manufacturer should verify important factors such as wavelength range, brightness, power use, heat control, electrical safety, and operating life. Good testing can identify weak connections, uneven illumination, excess heat, or control errors before products reach customers. For buyers, stable output supports reliable daily operation and a more predictable user experience. Clinics and salons can use equipment with greater confidence, while retailers and distributors can reduce returns linked to inconsistent quality. Industrial and agricultural users also benefit when lighting behaves similarly from one unit to the next. The red light manufacturer can provide sample reports, inspection records, production images, and test information to support purchasing decisions. Strong quality control does not eliminate every possible issue, but it reduces avoidable risk and gives buyers clearer evidence that the product is ready for its intended environment.
Scalable Supply and Responsive Business Support

Scalable Supply and Responsive Business Support

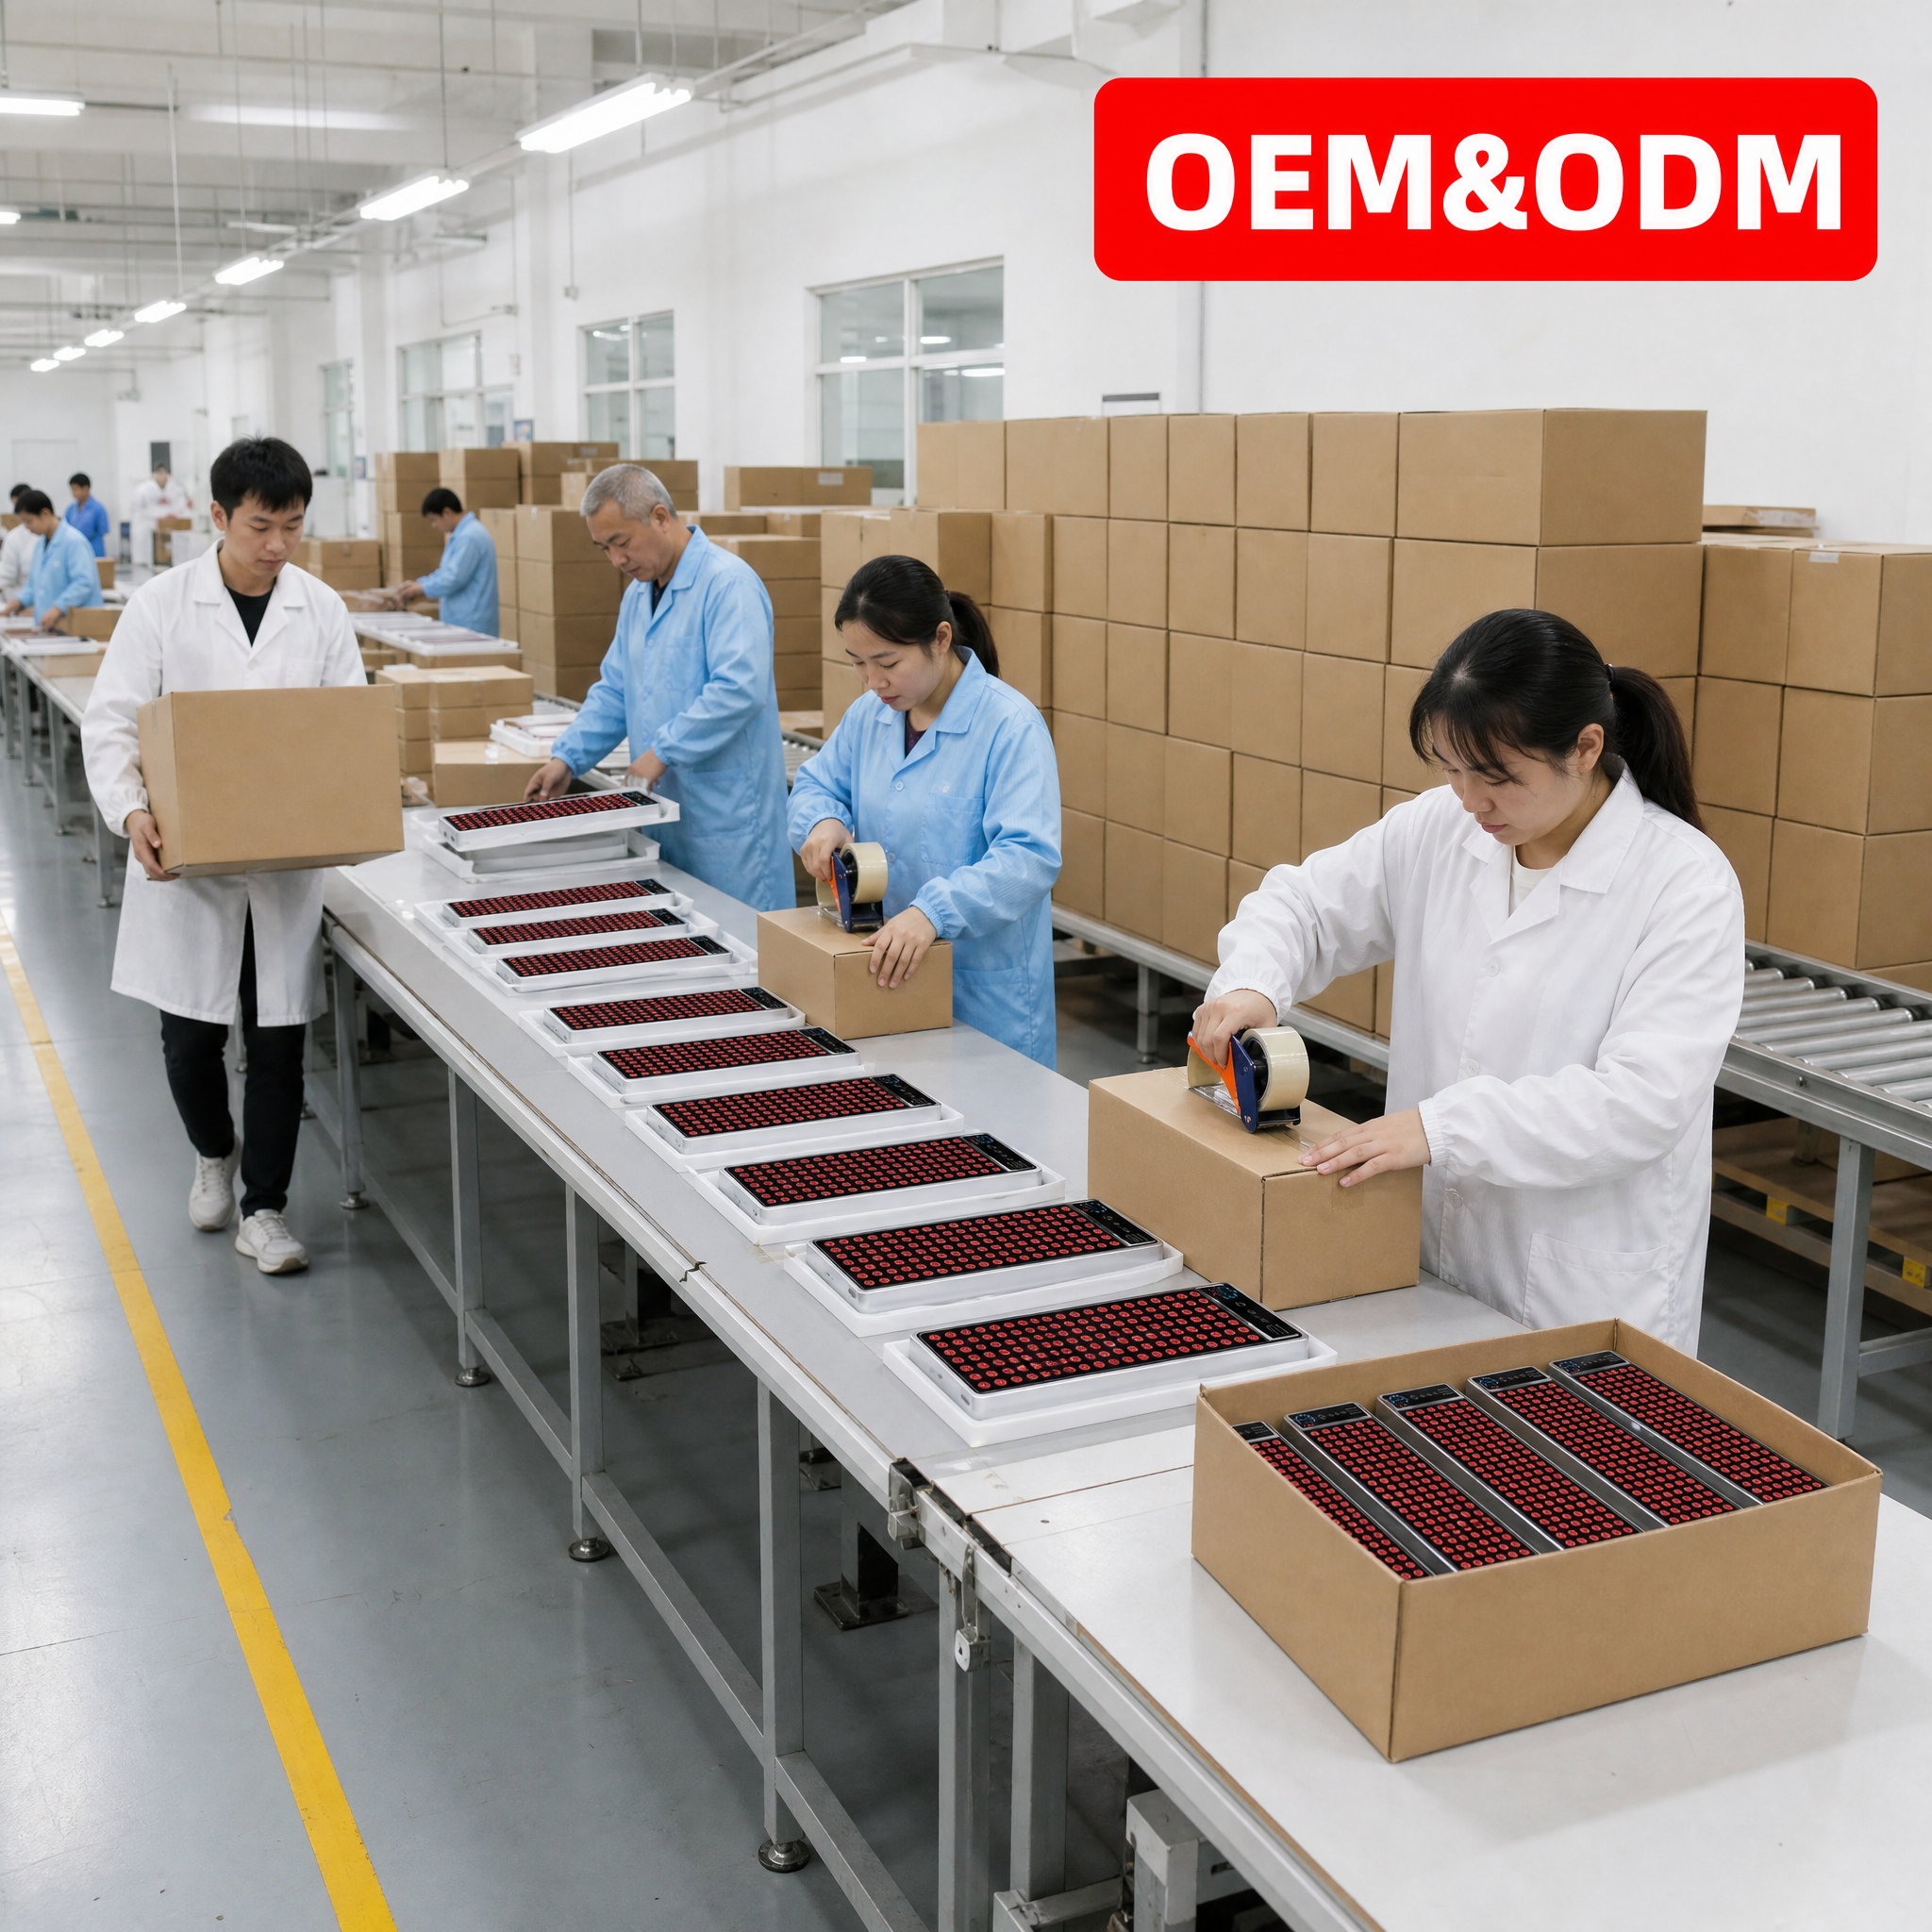
A dependable red light manufacturer supports customers beyond the first shipment. The red light manufacturer can help with sample development, order planning, packaging, replacement parts, shipping coordination, and future product updates. This support is valuable for both established companies and new brands testing demand. Scalable production allows a buyer to begin with a manageable quantity and increase volume as sales grow. The supplier can maintain the approved design while improving scheduling and material planning for repeat orders. That approach helps avoid unnecessary inventory and limits the disruption caused by changing suppliers too often. Responsive communication also makes it easier to resolve technical questions, confirm specifications, and respond to market feedback. A capable red light manufacturer may offer several business models, including standard purchasing, OEM production, private labeling, and contract development. Buyers can select the level of support that matches their resources. The result is a more practical supply relationship, with clearer responsibilities, better planning, and a stronger foundation for long-term commercial growth.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Mobile
Message
0/1000