medical red light factory
A medical red light factory designs, develops, tests, and produces red and near-infrared light equipment for professional healthcare, rehabilitation, beauty, and wellness use. The medical red light factory manages the full production process, from LED selection and optical design to assembly, quality inspection, packaging, and shipment. This integrated approach helps buyers receive consistent products from one accountable source.
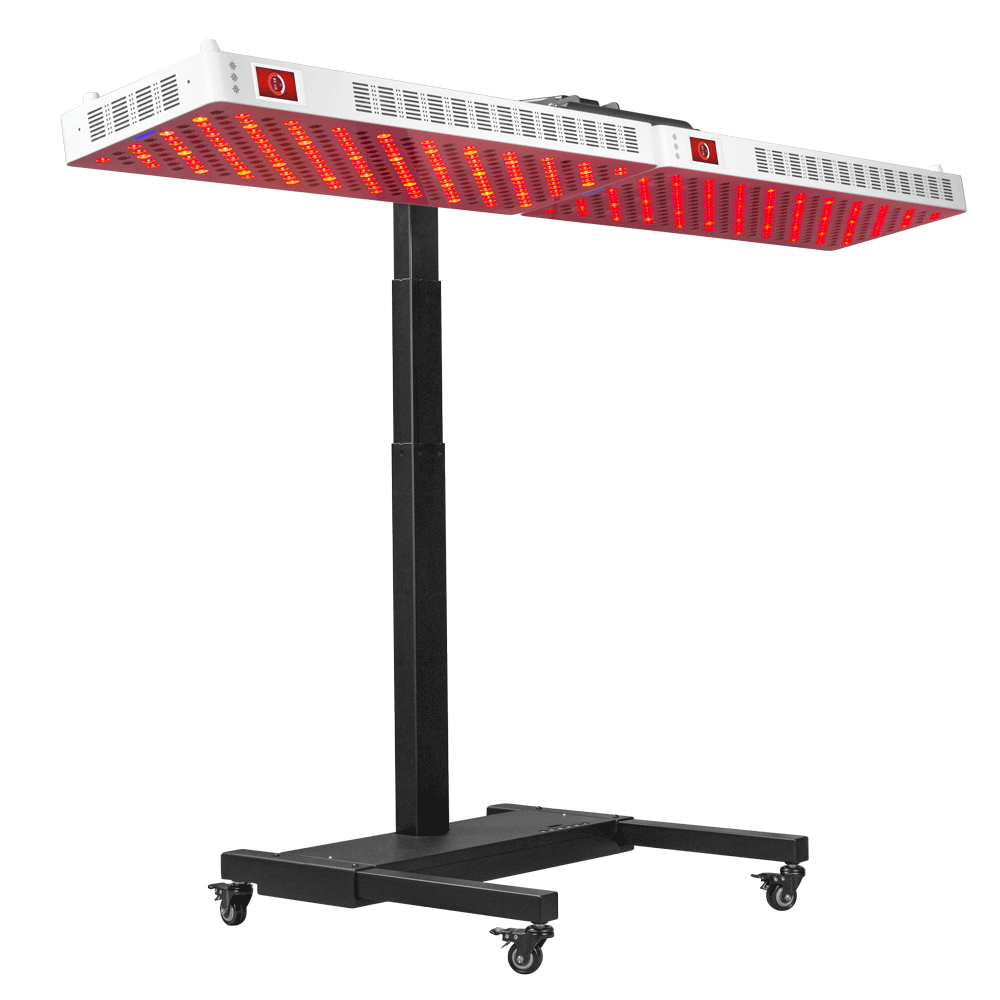
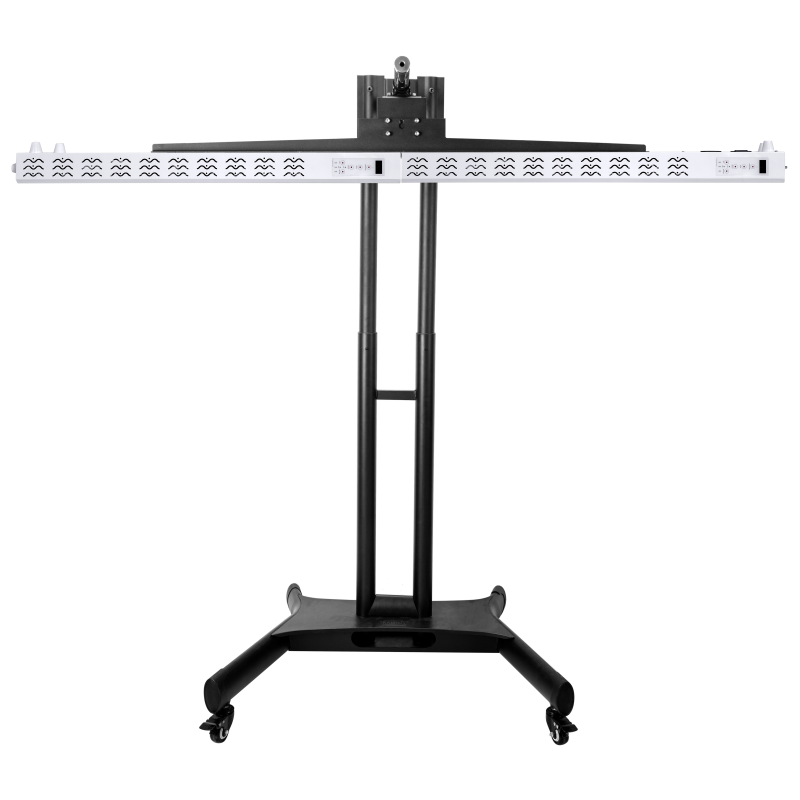
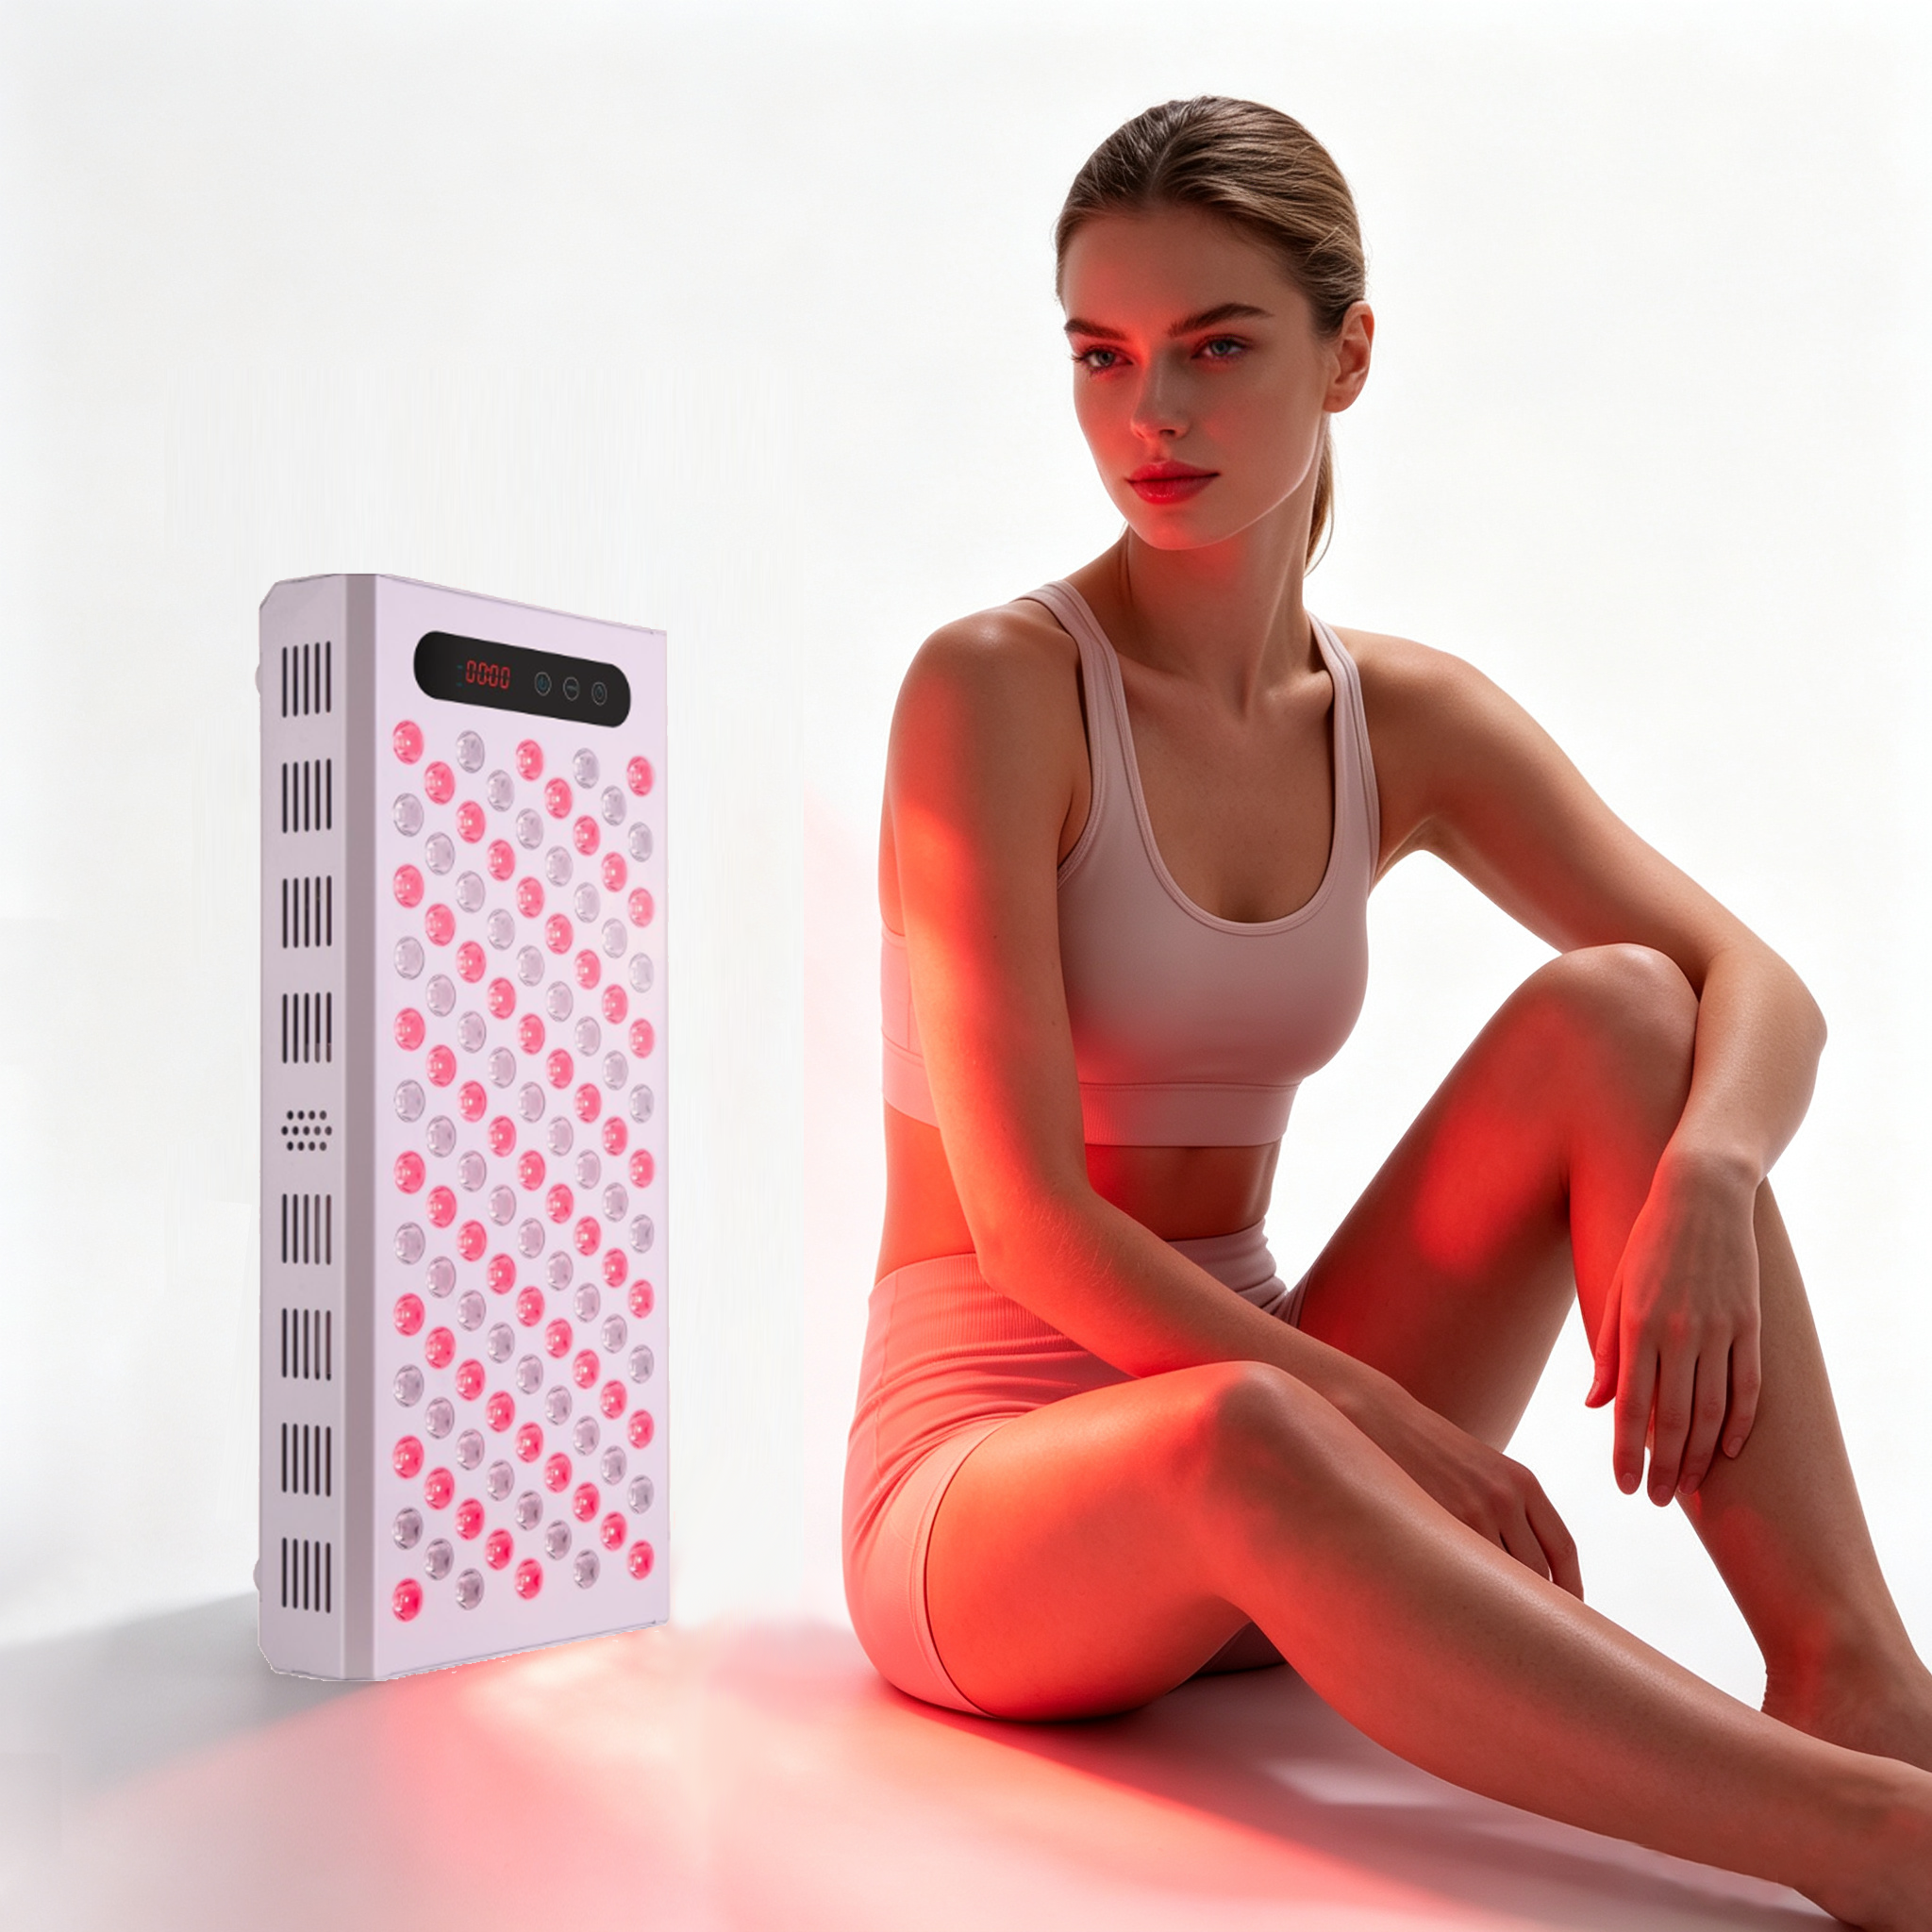
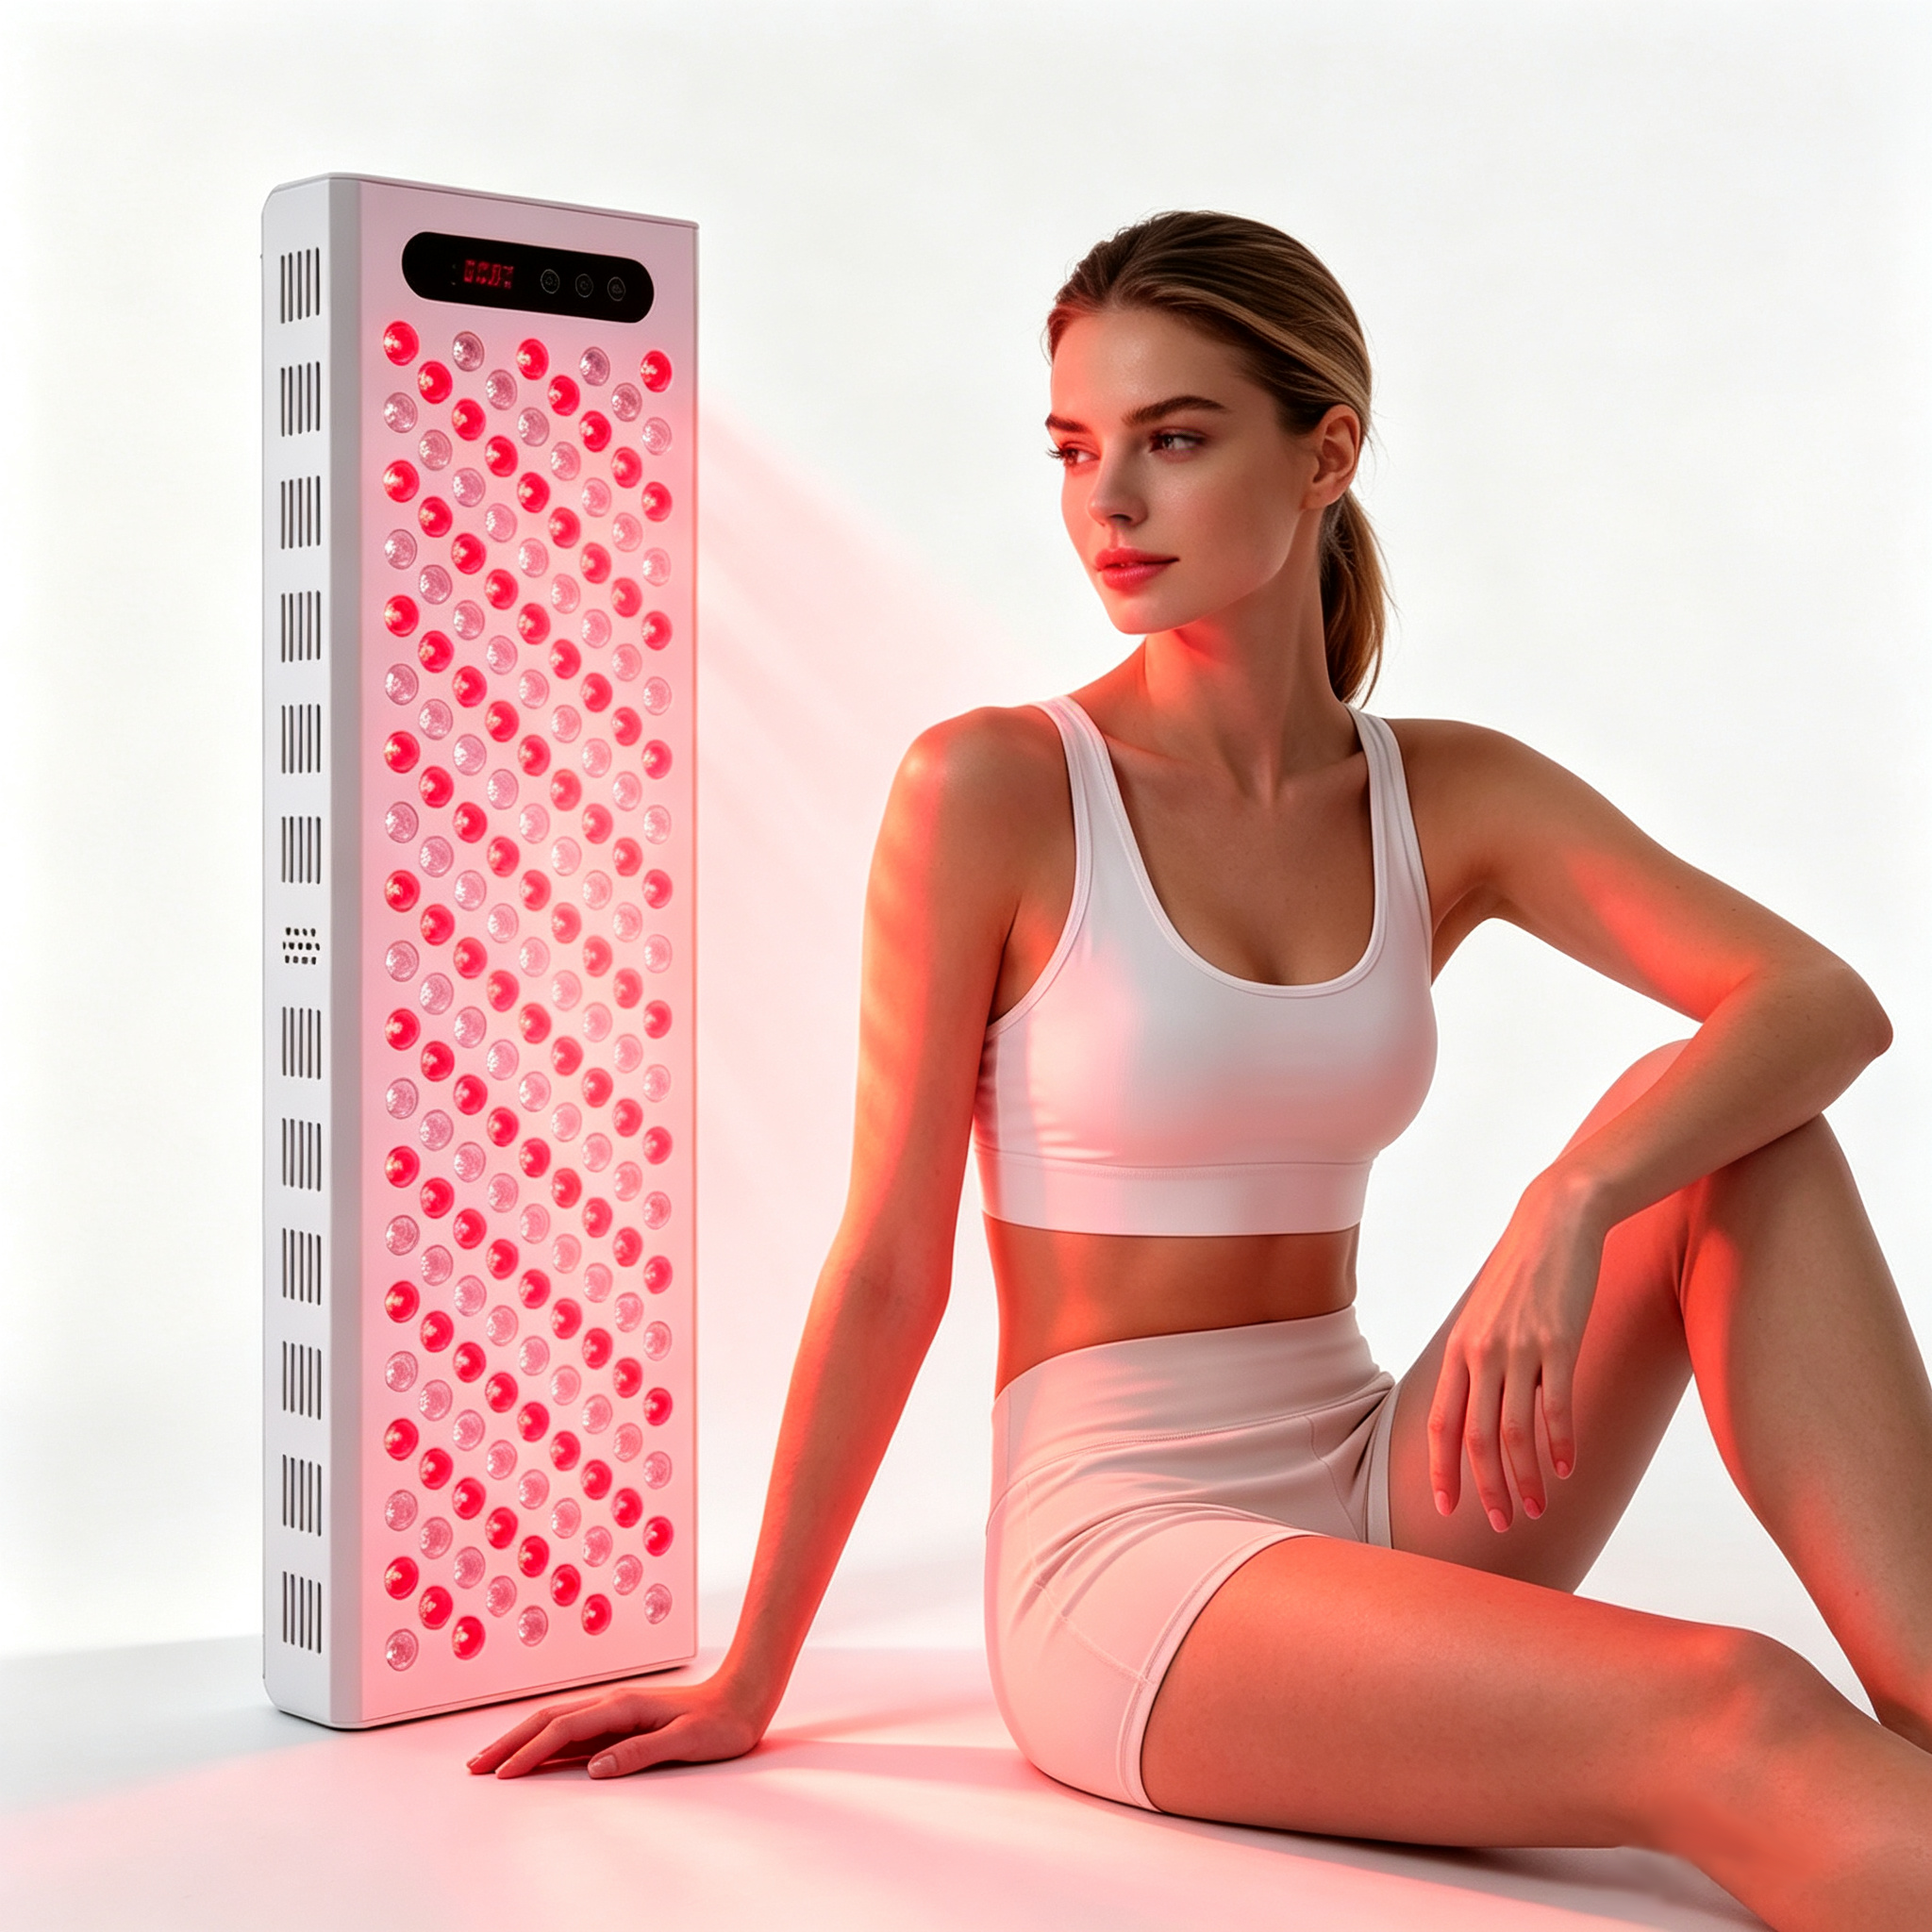
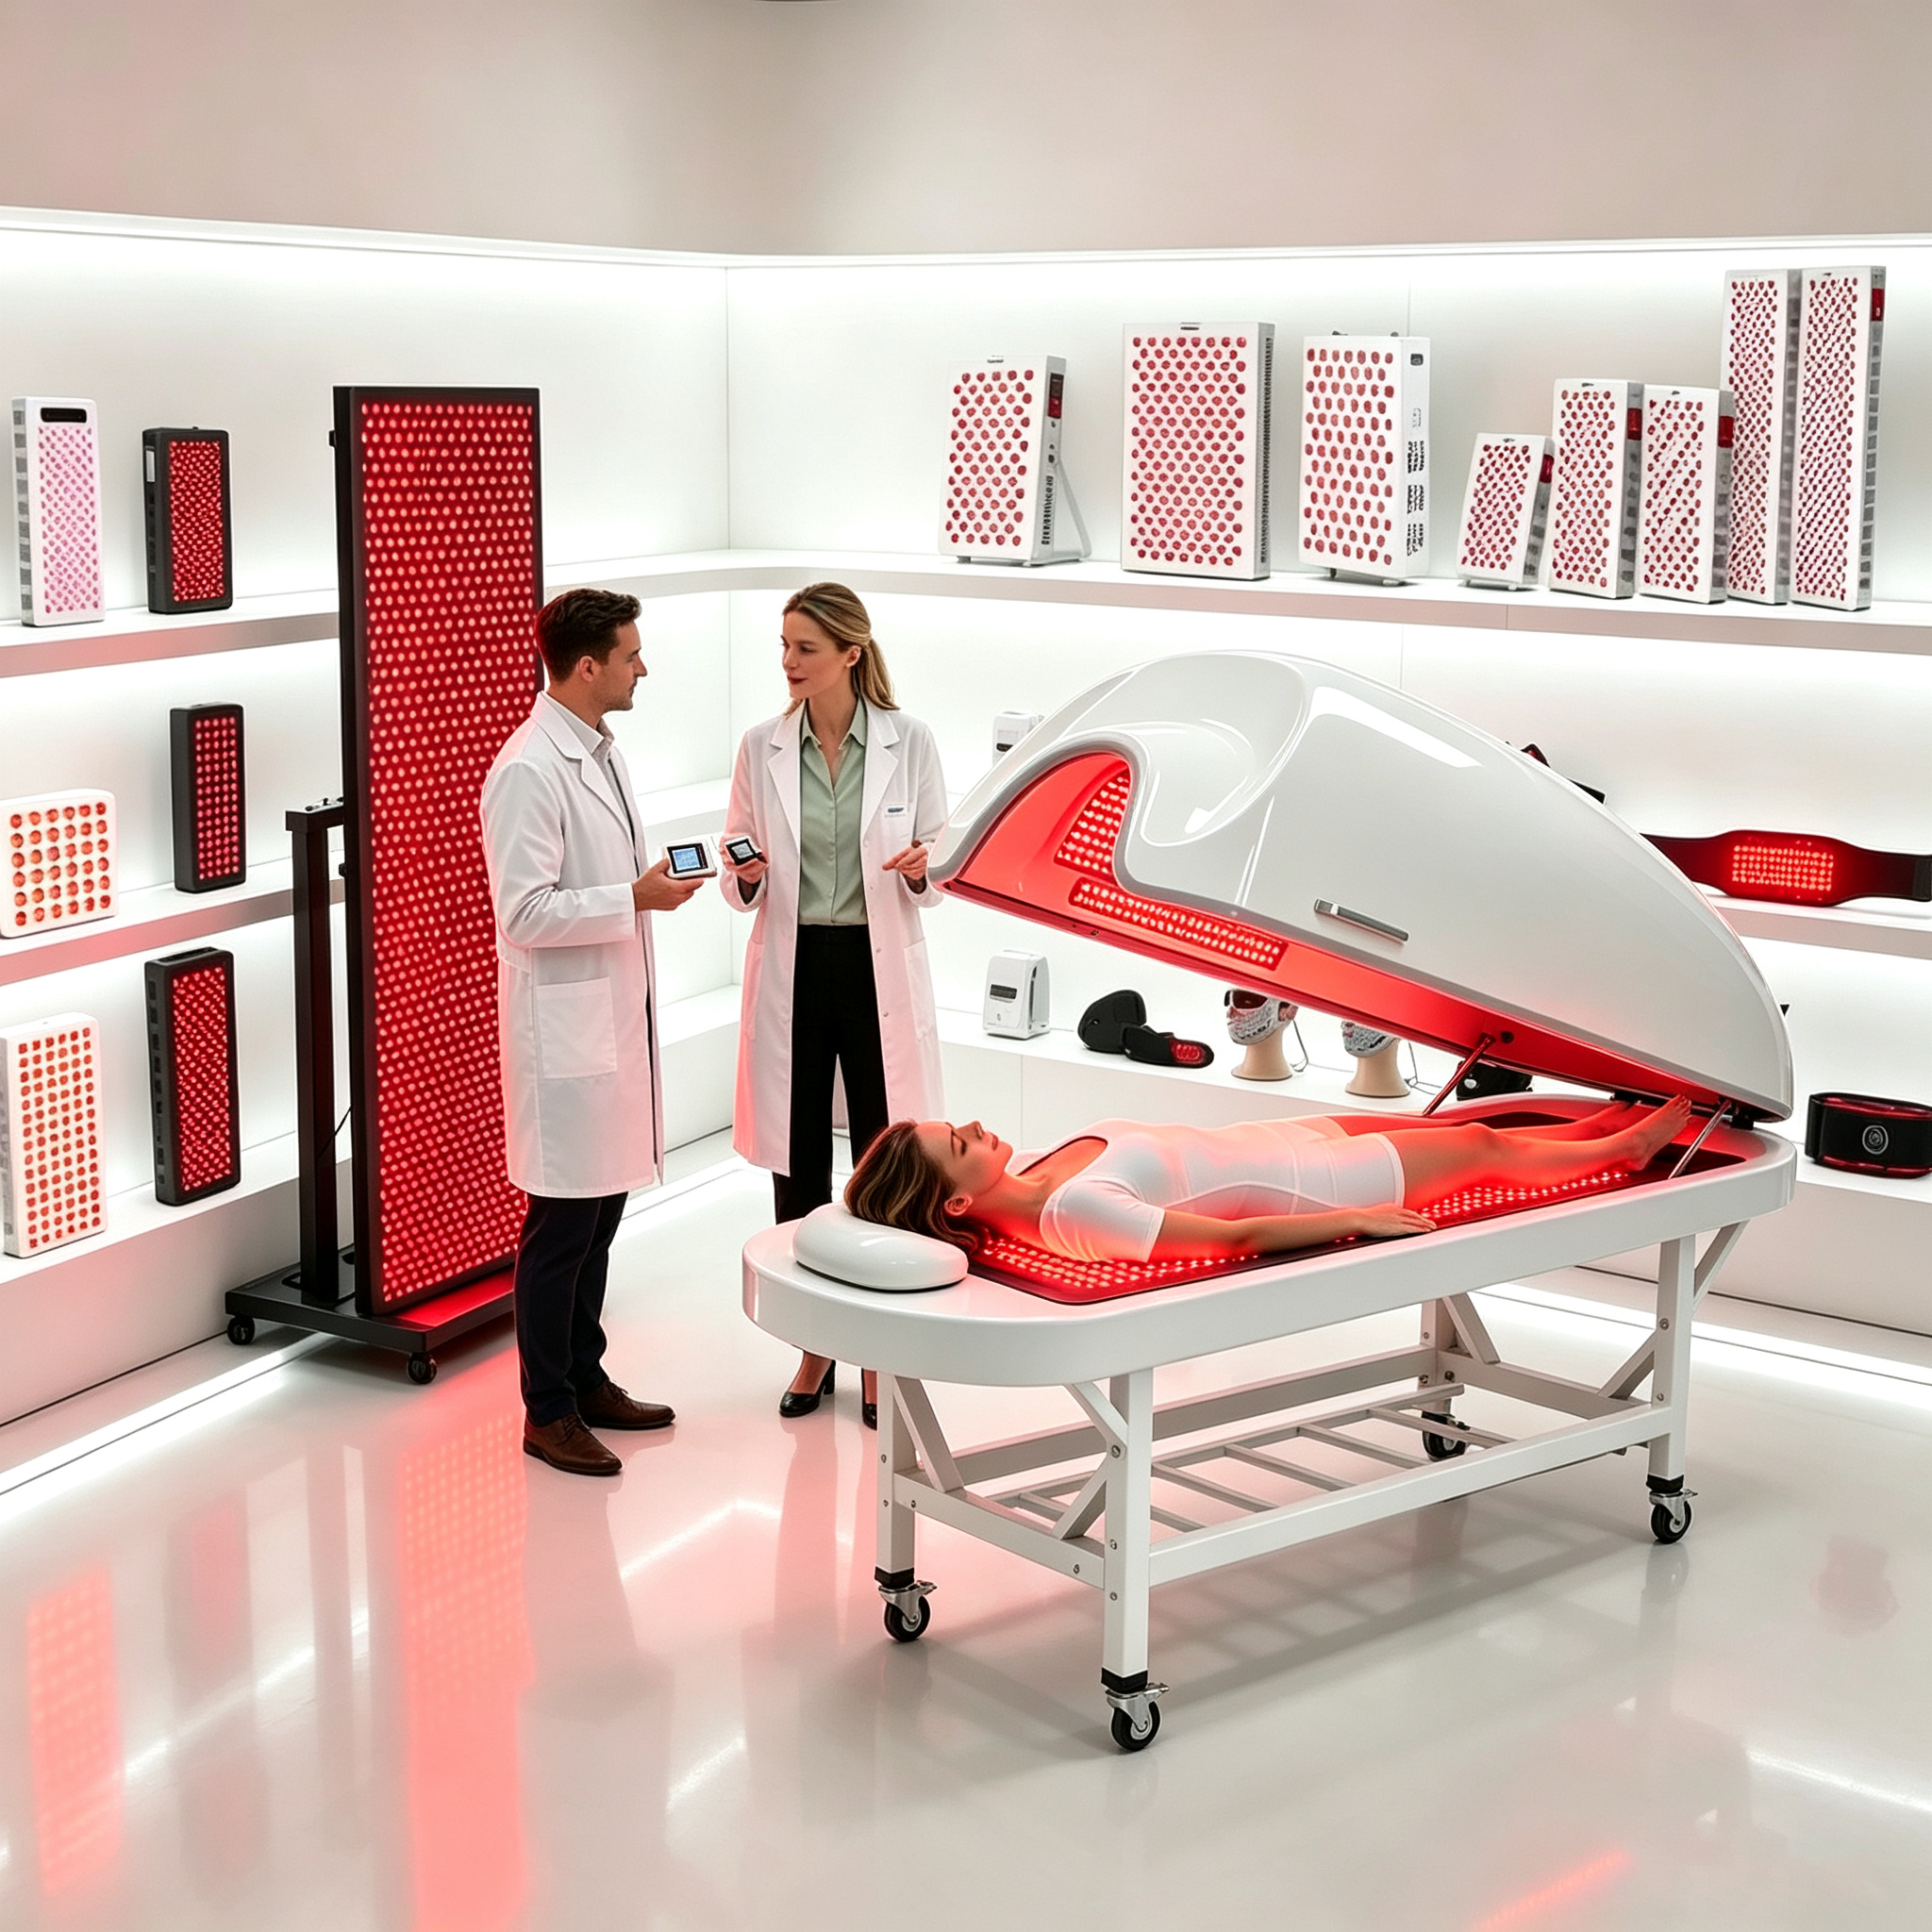
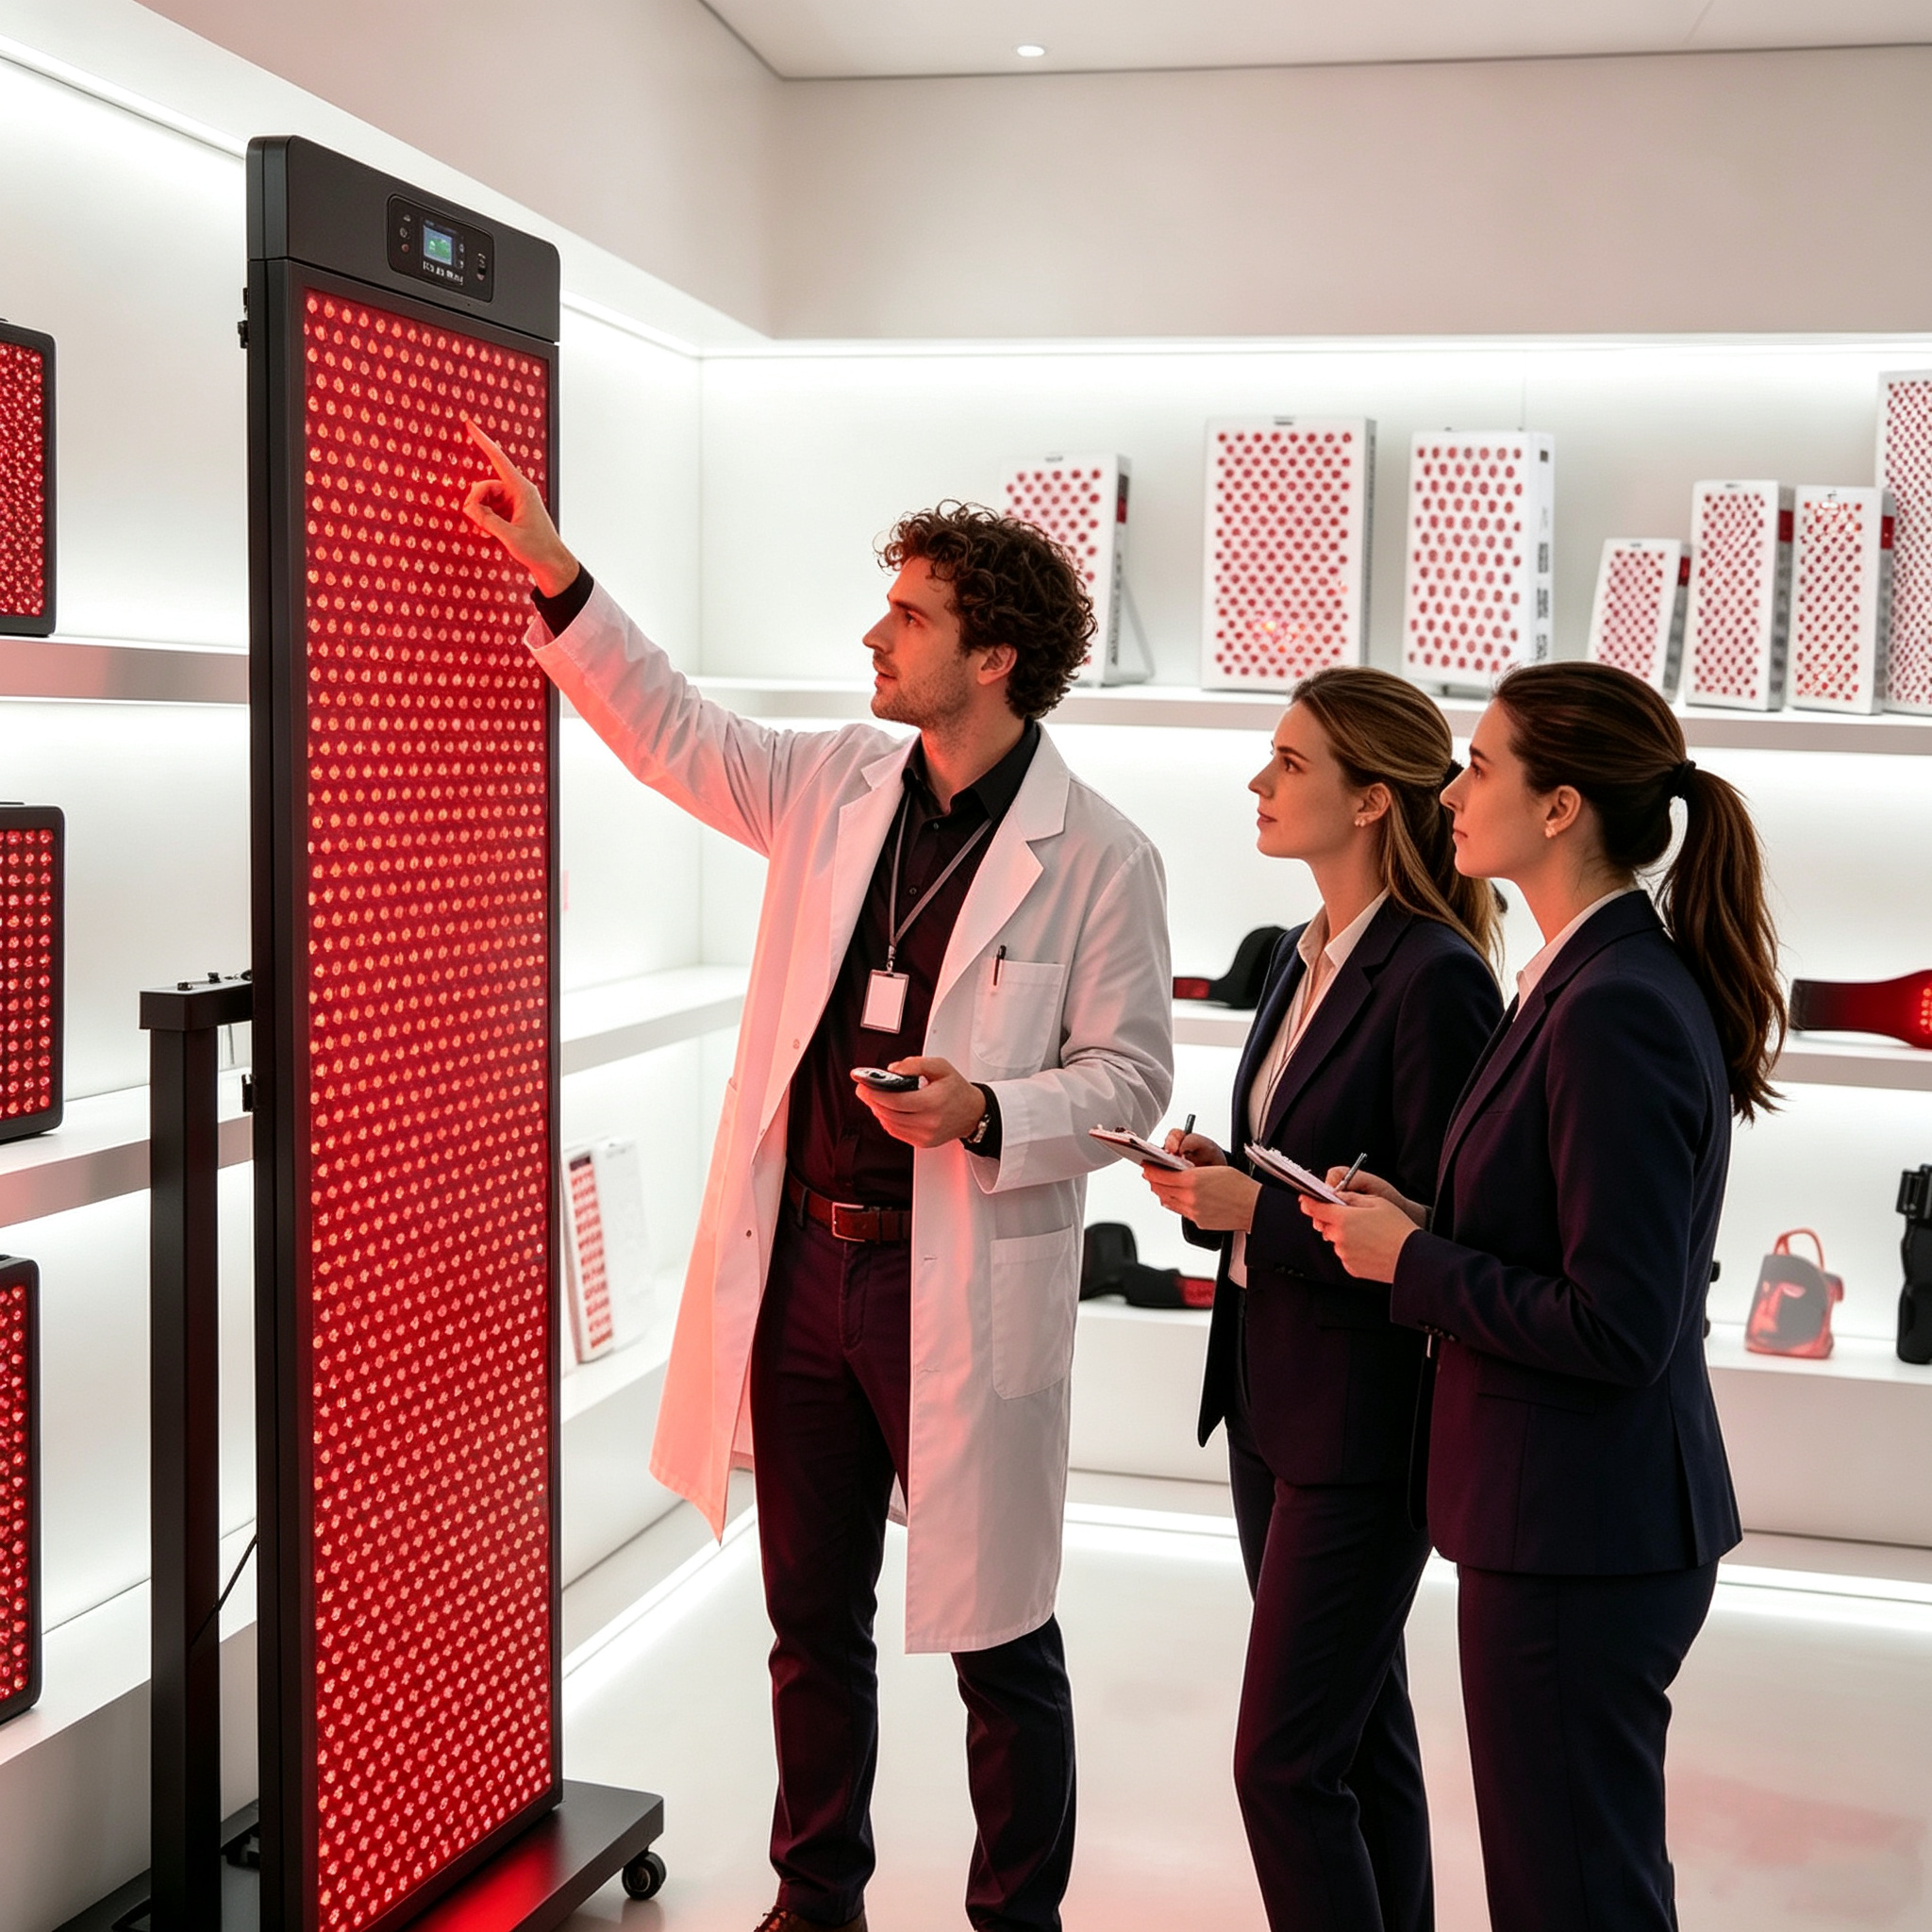
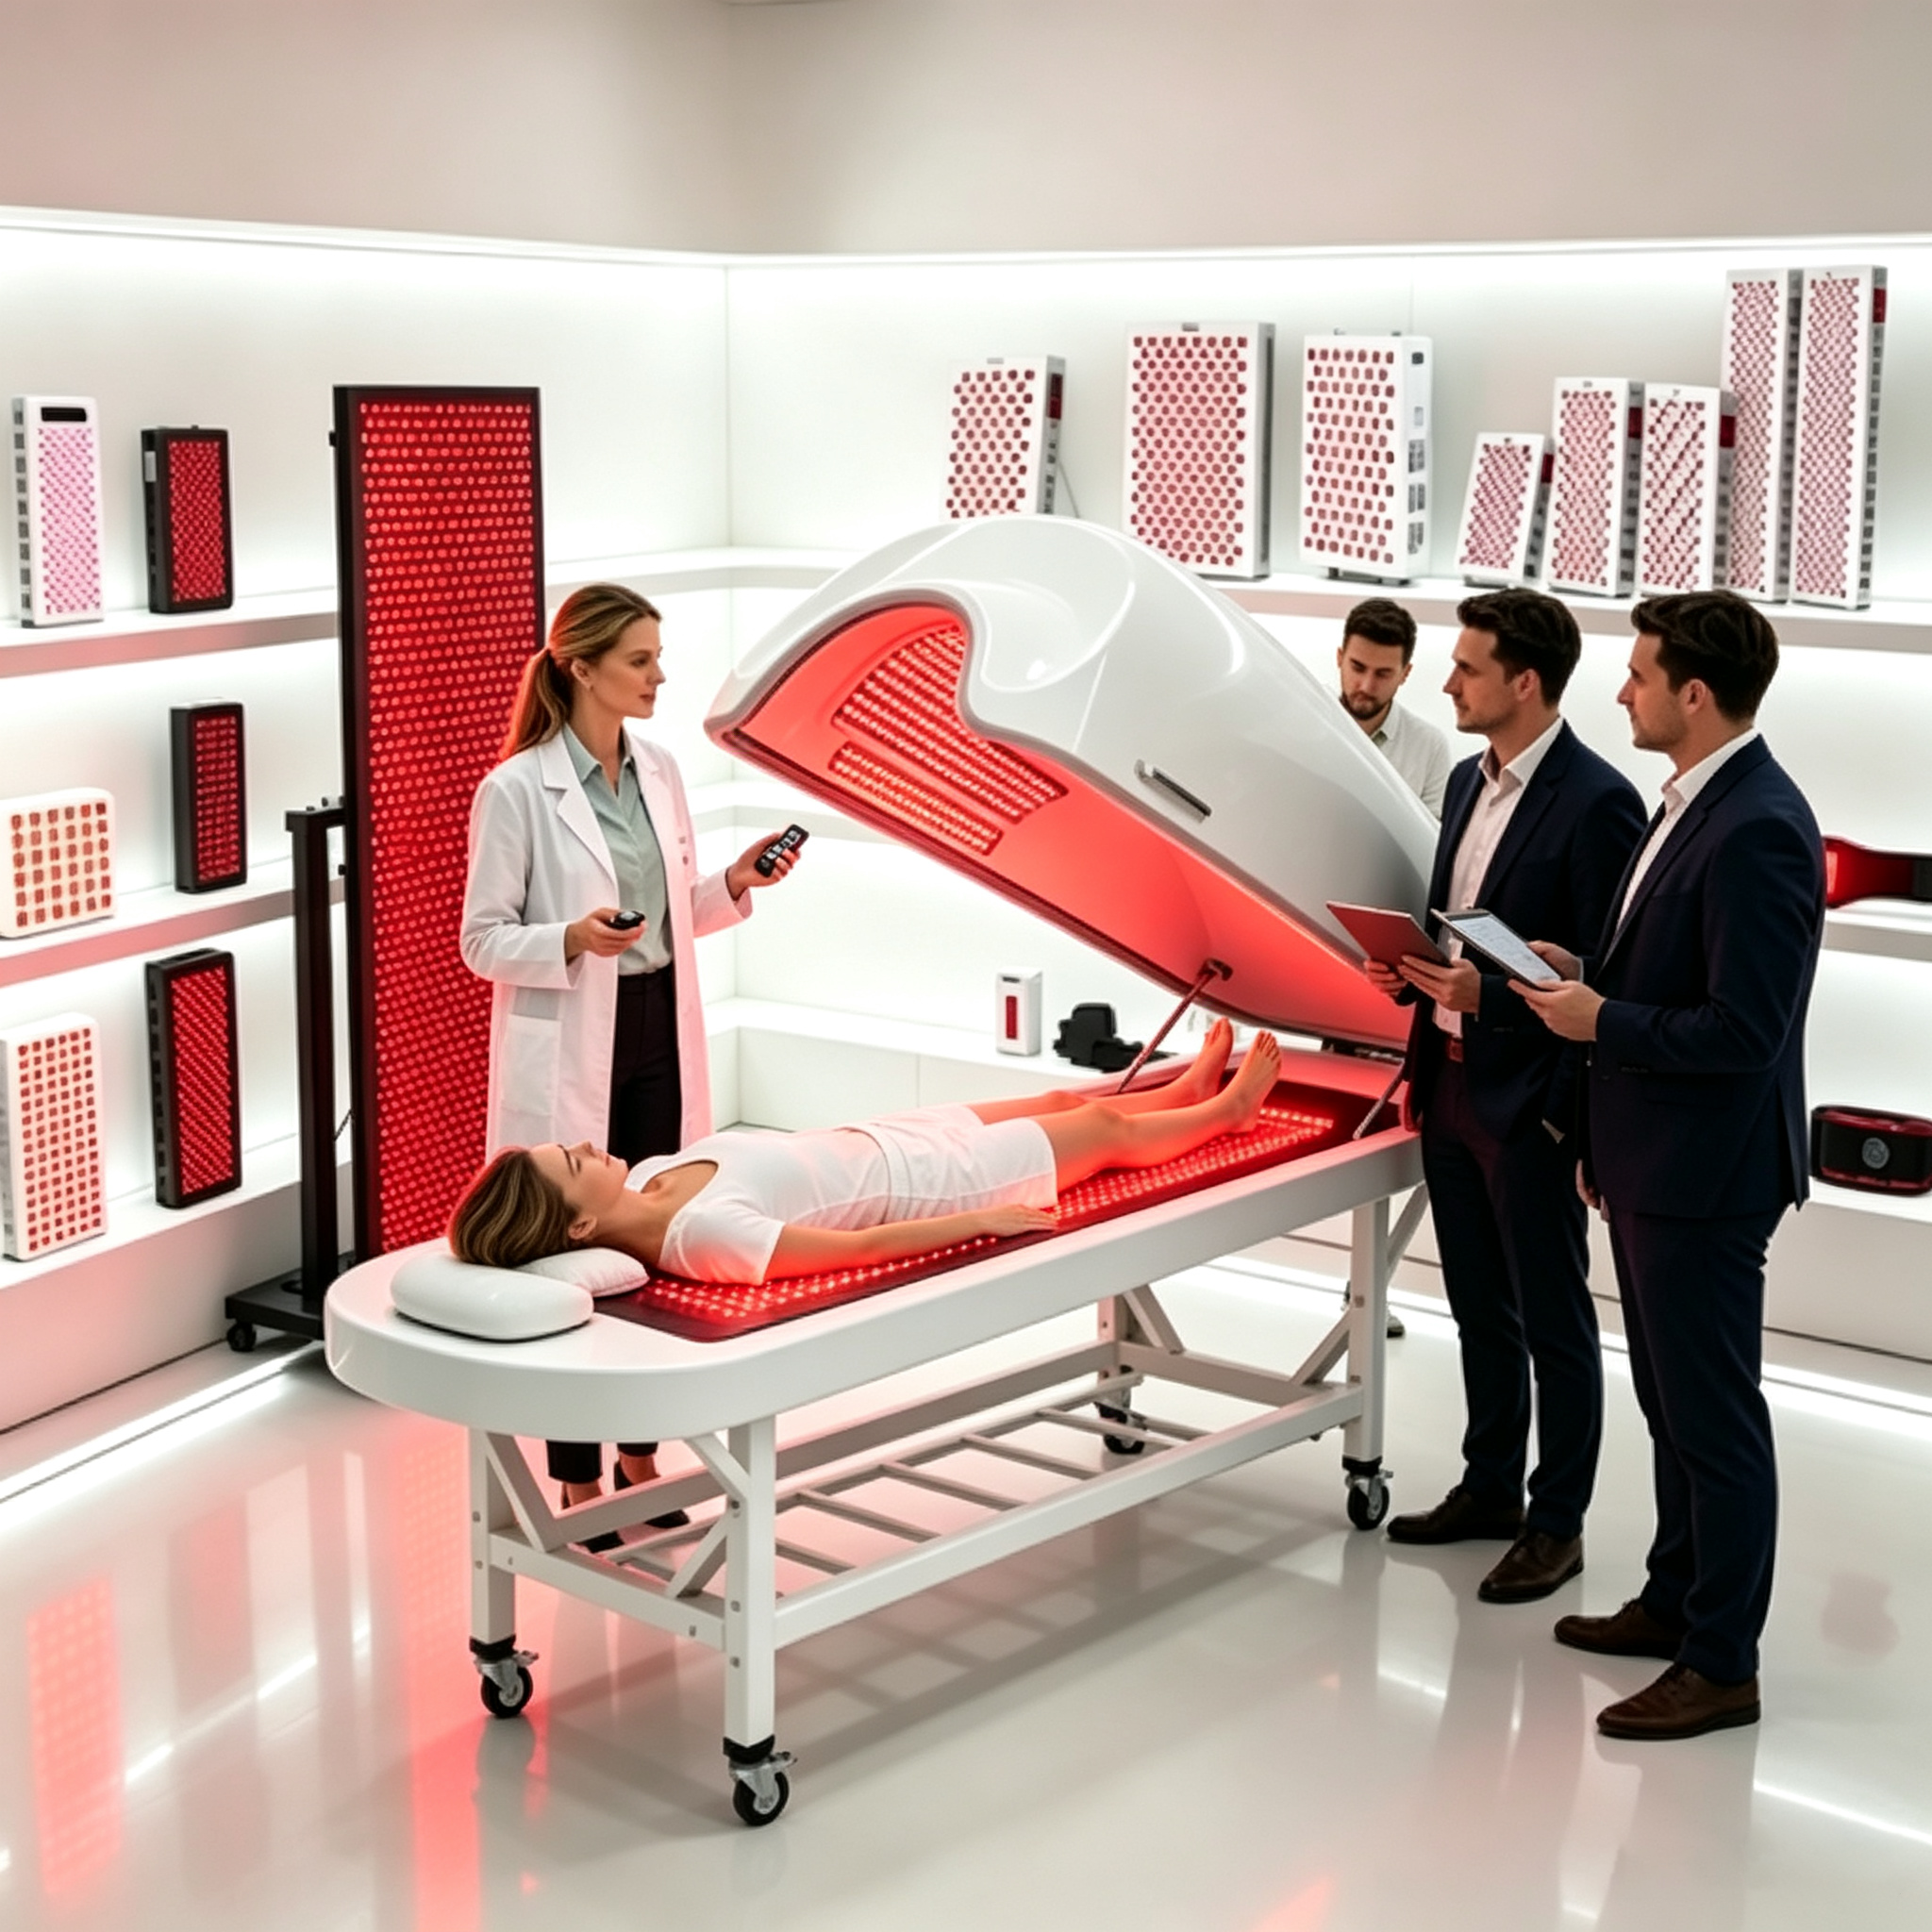
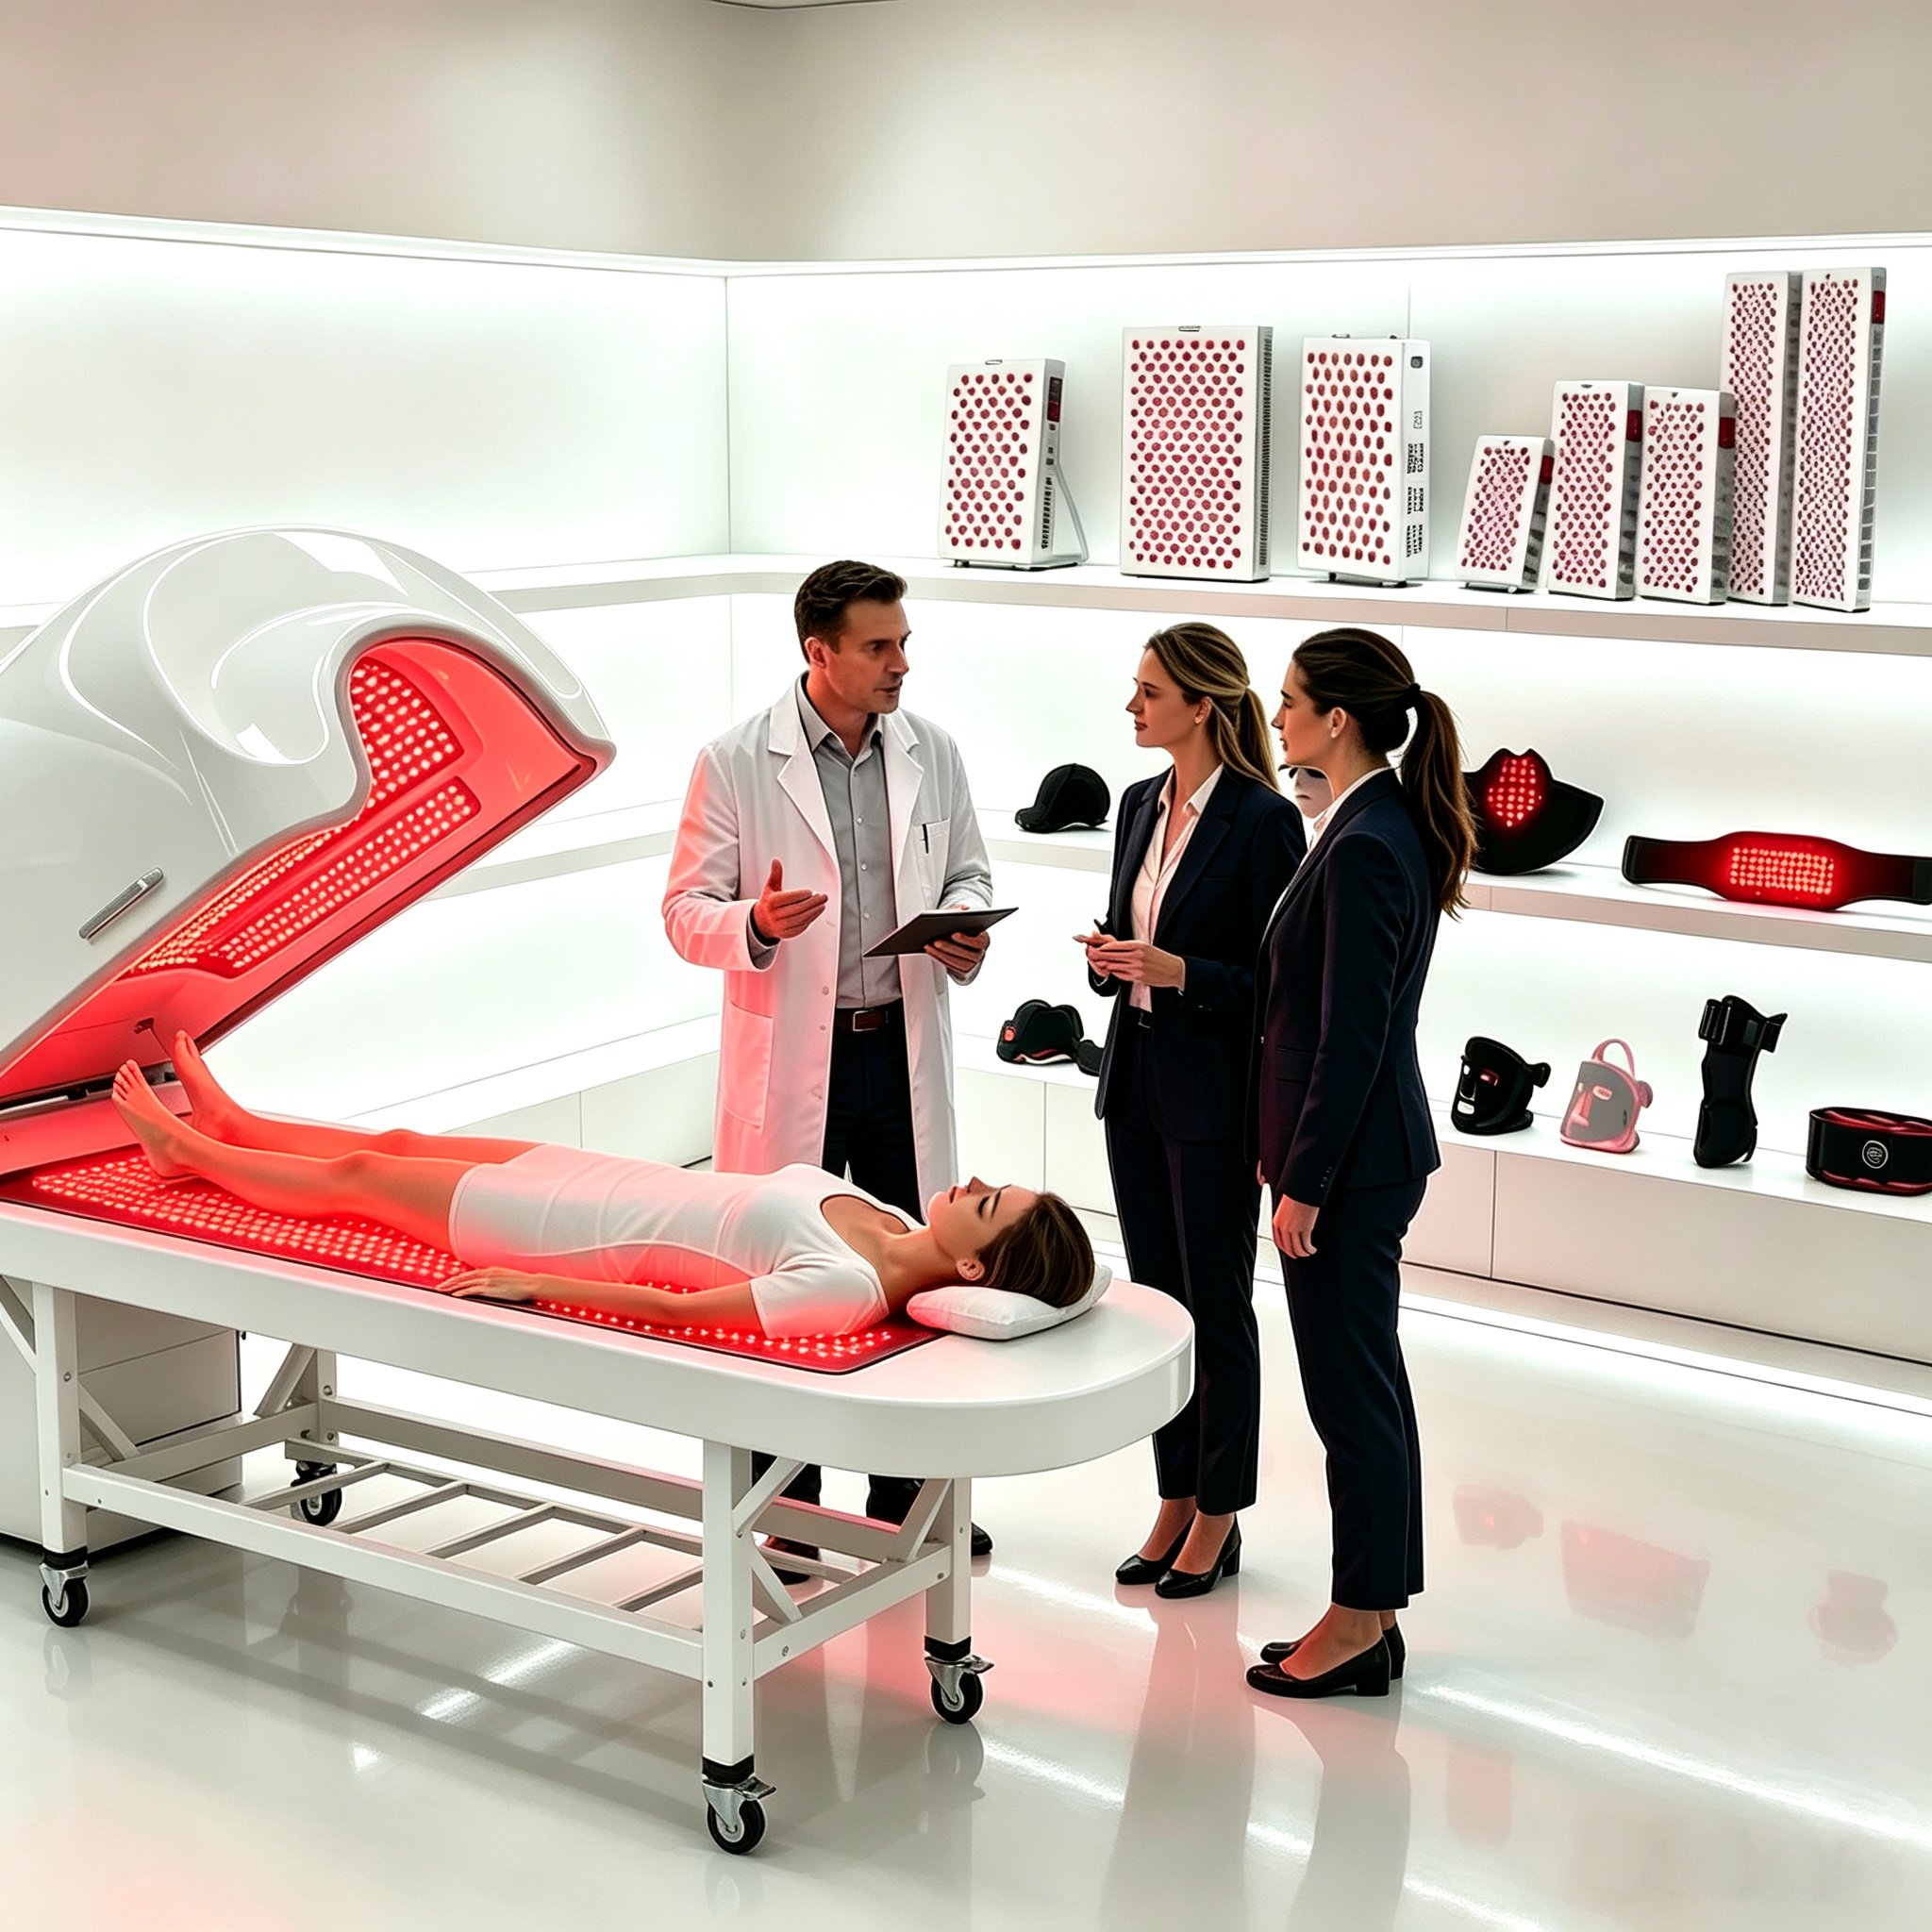
The medical red light factory typically supplies panels, floor-standing systems, flexible belts, handheld devices, face masks, and targeted treatment lamps. Each medical red light factory can adjust wavelength combinations, treatment area, power output, timer settings, housing materials, and control methods to suit a specific application. Common wavelength options include visible red light and near-infrared light, selected for different surface and deeper-use requirements.
A reliable medical red light factory uses calibrated LEDs, thermal management, protective housings, stable power supplies, and user-friendly controls. Many facilities add digital displays, preset programs, adjustable intensity, cooling systems, treatment timers, and remote or app-based operation. The medical red light factory also applies electrical safety checks, light output testing, aging tests, and final inspections before delivery.
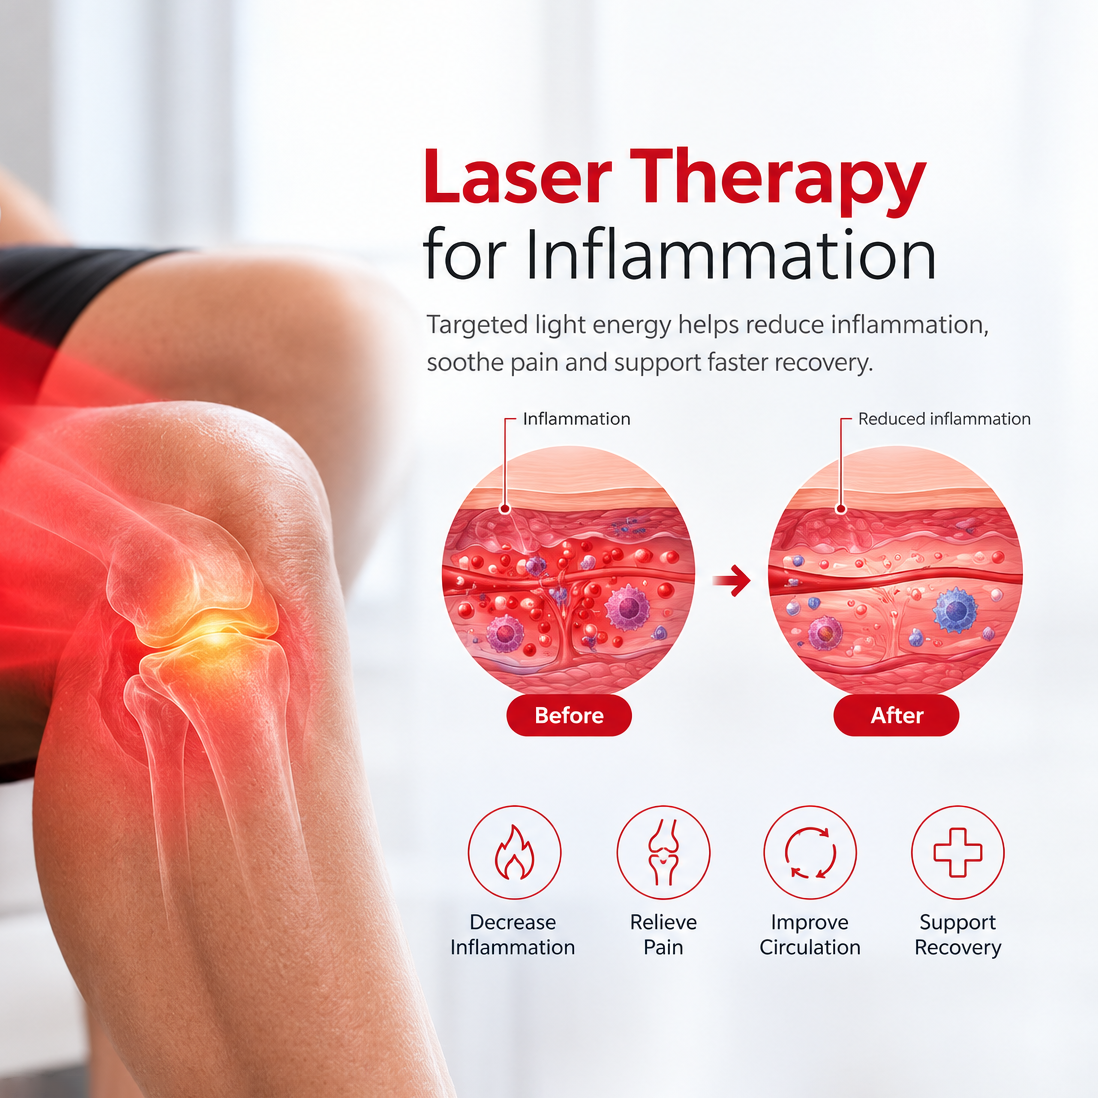
Applications include clinic-based light therapy, physical recovery programs, skincare services, sports facilities, home wellness, and private-label product lines. The medical red light factory can support small pilot orders as well as larger OEM and ODM programs. Its main role is to turn a treatment concept into a dependable, scalable device that is easier to operate, maintain, brand, and distribute.